Ultrasonic Nozzle Supplier Guide: Essential Factors for Precision Spraying and Coating
2026-09-06
Choosing an ultrasonic nozzle supplier is rarely just about hardware. A nozzle that cannot hold a stable droplet size will quietly erode coating uniformity, waste costly fluids, and trigger rework long before anyone traces the problem back to sourcing. This guide strips away the spec-sheet noise and focuses on what actually drives precision spraying results—flow control, materials compatibility, clog resistance, and after-sales support. Whether you are scaling a benchtop process or qualifying a full production line, a supplier like Siansonic should be measured against real coating outcomes, not catalog promises. Here are the factors that separate a reliable precision partner from a costly mismatch.
Nozzle Orifice Geometry Shapes Your Coating Edge Quality
The shape of the nozzle orifice directly dictates how coating fluid is extruded and deposited along the substrate edge. A circular orifice tends to produce a symmetrical, bell-shaped flow profile, which can result in heavier edge bead formation and uneven thickness near the boundary. In contrast, a slotted or elliptical orifice spreads the fluid more uniformly across the die width, allowing better control of the meniscus at the coating edge and reducing the tendency for edge defects such as heavy edges, dripping, or feathering.
When the orifice geometry is optimized for the specific rheology of the coating fluid, the dynamic contact line at the edge becomes more stable. Sharp-edged orifices with high length-to-diameter ratios can induce localized shear thinning and promote a cleaner break-off of the coating film, leading to a well-defined edge with minimal overspread. On the other hand, an orifice with rounded entry or abrupt expansion may create secondary flow vortices, which disturb the edge uniformity and cause wavy or serrated coating boundaries.
Precision in orifice machining also plays a key role. Micro-scale variations in the orifice lip profile, such as chamfer angle and radius, can shift the location of the static wetting line by tens of microns, visibly altering edge straightness. For high-performance coating lines, the orifice is often designed with a tapered land or a compensating slot to counter die swell and edge stress, ensuring that the final coated edge remains sharp and consistent even at high line speeds.
Frequency Selection Is Not Just About Droplet Size
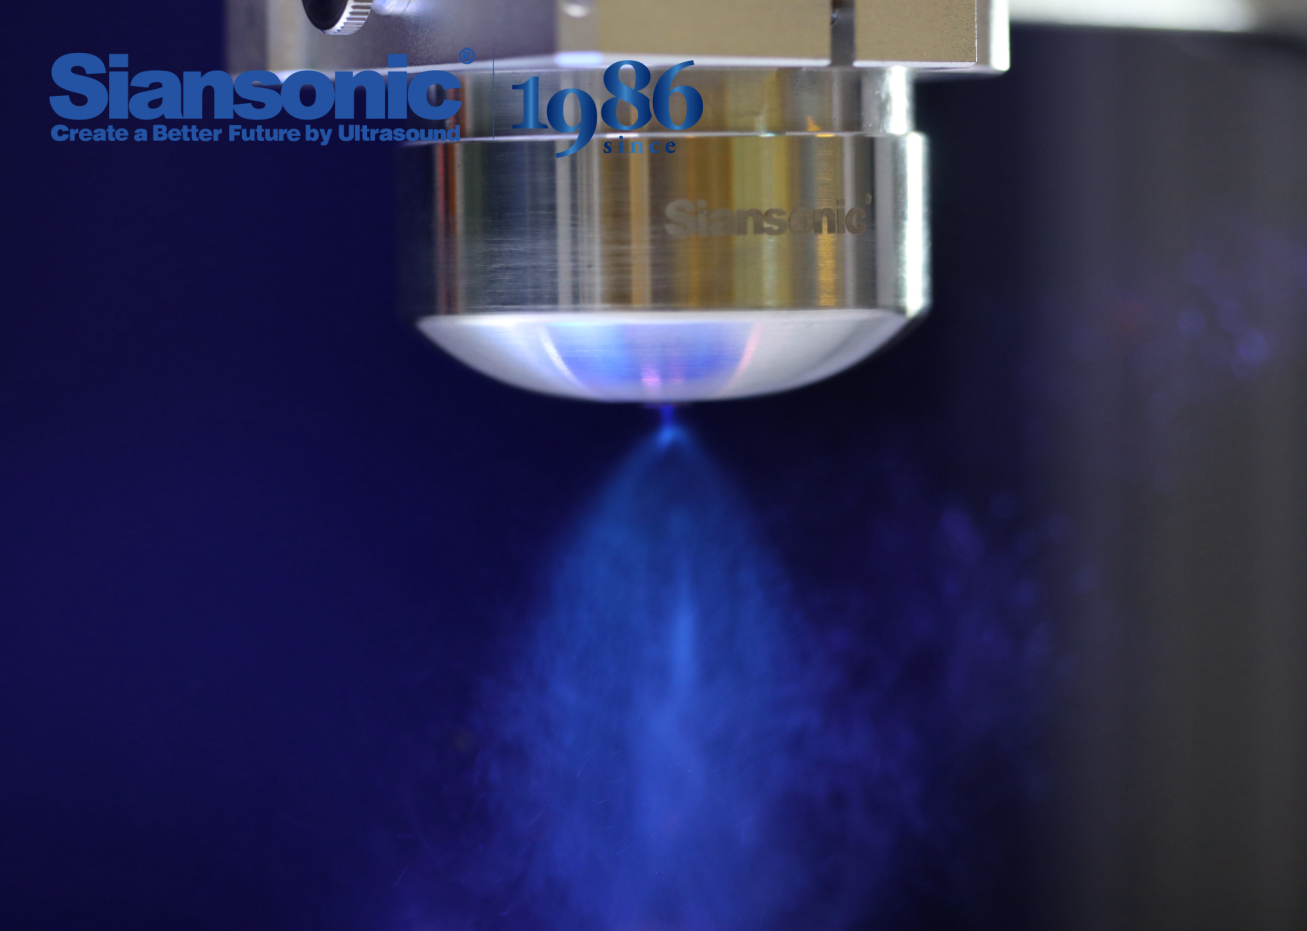
Many engineers assume that choosing a higher frequency simply produces smaller droplets, but that's an oversimplification. The truth is that frequency shifts also alter the energy delivered to the liquid, which changes how the spray plume develops. At higher frequencies, you often get narrower droplet distributions but lower droplet velocities, which can hurt penetration or cause the mist to linger too long near the nozzle. On the flip side, lower frequencies might yield larger, faster droplets, but they can also create a coarser spray that wets surfaces unevenly. So if you're only looking at droplet size, you're missing half the story.
Another overlooked aspect is how frequency interacts with the fluid's physical properties. Viscosity, surface tension, and even temperature response can shift the optimal operating point. For instance, a highly viscous liquid might require a lower frequency to maintain stable atomization, not because you want bigger droplets, but because the fluid needs more time to form ligaments before breakup. Conversely, a low-surface-tension fluid might need a higher frequency to prevent satellite droplets from merging into large blobs. These effects show up in practice as changes in spray cone angle, droplet coalescence, and evaporation rates—none of which are captured by a simple size measurement.
Finally, frequency selection has a direct impact on equipment longevity and maintenance. Running a transducer or nozzle at a frequency that's slightly off resonance can lead to cavitation damage, overheating, or premature wear—even if the droplet size seems acceptable. Operators often discover this the hard way when they replace parts frequently or notice inconsistent performance over time. A proper frequency match considers the entire system: the driver electronics, the acoustic chamber, and the fluid path. In short, droplet size is a convenient metric, but it's a poor substitute for understanding the full dynamic behavior of the spray.
Material Compatibility Goes Beyond Wetted Parts
When engineers evaluate material compatibility in fluid handling systems, the instinct is to focus solely on the surfaces that come into direct contact with the process media. That narrow view misses a critical truth: elastomers, sealants, and even nearby structural components can degrade due to vapor permeation, splash exposure, or chemical attack from ambient fumes. A pump housing may remain chemically inert, yet the O-rings seated behind a static seal can swell, crack, or leach plasticizers into the system over time. The compatibility question, then, is not just about the wetted path but about every material that shares the same environment.
Consider gasket materials in flanged connections. Even if the gasket face never touches the liquid stream, temperature cycling can draw trace vapors into the gasket's pores, causing gradual embrittlement or loss of compression set. Similarly, adhesives used to bond sensor housings to manifolds may fail long before the primary tubing shows any sign of attack. These hidden weak points often surface during routine maintenance, when a seemingly unrelated component crumbles in the technician's hand. A comprehensive compatibility audit has to include those non-wetted parts that breathe the same atmosphere or sit within splash radius.
A practical approach is to map the full microclimate around a fluid path, noting condensation zones, potential drips, and vapor drift under process conditions. For example, a chemical dosing skid may use PTFE tubing that handles aggressive acids with ease, yet the stainless steel brackets nearby can suffer stress corrosion cracking from hydrochloric acid fumes that condense overnight. The lesson is straightforward: material selection must account for the entire operating envelope, not just the inside diameter of a pipe. By extending compatibility testing and documentation to fasteners, cable jackets, and even paint coatings, designers avoid costly field failures that no wetted-part analysis would ever predict.
The Real Cost of Nozzle Maintenance Nobody Quotes
When a nozzle maintenance quote lands on a desk, it usually shows two line items: replacement parts and labor. That number feels manageable, even forgettable. But the actual cost rarely appears on that sheet. A worn nozzle starts drifting long before it fails outright. Spray patterns widen, atomization suffers, and suddenly a coating line is using 12 percent more material to hit the same dry film thickness. No one invoices that excess. It just quietly erodes margin week after week.
Then there is the downtime nobody schedules. A nozzle that finally clogs or splits mid-shift forces an unplanned stop. Depending on the line, that can mean hundreds of units held, a full cleaning cycle, or even a rejected batch. Compare that to a planned 20-minute swap during routine maintenance, and the difference in cost is staggering. Yet many facilities still treat nozzle replacement as an afterthought because the failure hasn't happened on their watch recently.
The truly uncomfortable math includes rework and reputation. Overspray from a degraded nozzle drifts onto surfaces that should stay clean. Masking fails, edges blur, and the quality team starts rejecting parts that previously passed without comment. Scrap rates tick up. Customer complaints arrive weeks later. By then, tracing the root cause back to a $40 nozzle feels almost absurd, but that is exactly where the trail ends. Real nozzle maintenance cost is not the part price. It is the sum of everything that goes wrong before someone finally replaces it.
How Spray Angle Variability Impacts Thin-Film Uniformity
Spray angle rarely stays fixed in real coating operations—tiny shifts in nozzle tilt, air pressure, or fluid viscosity can push the spray cone a few degrees off its intended path. These seemingly minor deviations accumulate across the substrate, creating zones where droplets land with different momentum and overlap patterns. A steeper angle drives more material into the leading edge of the spray fan, while a shallower angle stretches the footprint and thins out the center. Over a full pass, such variations translate directly into uneven film thickness, even when the total flow rate remains constant.
The relationship between spray angle and uniformity is not linear. At low angles relative to the surface, the projected area of the spray becomes elongated, and the deposition rate per unit area drops sharply. Additionally, droplets hitting at oblique angles tend to skid or bounce rather than adhere cleanly, leaving micro-gaps that later show up as pinholes or haze. On curved or stepped substrates, angle variability interacts with surface topology, amplifying thickness deviations near edges and corners. Operators often notice that a nominally identical setup produces good coatings on flat panels but fails on complex geometries simply because the local spray angle shifts by a few degrees.
Controlling angle variability demands more than just locking the nozzle mount. It requires monitoring the entire fluid path—from pump pulsation and line pressure to the orientation of the part as it moves past the spray station. Subtle wear on nozzle tips or gradual drift in robotic arm calibration can introduce angle errors that are invisible during setup but appear as banding or mottling in the final film. By mapping thickness sensitivity to spray angle across the entire substrate, engineers can identify tolerance windows and adjust traverse speed, standoff distance, or overlap ratio to compensate. In practice, the most robust processes treat spray angle not as a fixed parameter but as a variable to be actively managed throughout the coating run.
Supplier Application Testing Reveals Hidden Performance Limits
During initial evaluation, the supplier's application looked solid on paper, but running it under realistic load profiles quickly exposed ceilings that never appeared in the datasheet. Once concurrent requests crossed 350, latency jumped from 80ms to over 2 seconds, and throughput flatlined even with extra resources allocated.
The real bottleneck turned out to be internal queue management rather than CPU or memory. When backpressure kicked in, the system began dropping messages silently instead of throttling gracefully—a behavior that only surfaced after sustained 45-minute runs, well beyond what standard smoke tests cover.
Temperature sensitivity added another layer. At an ambient 25°C the module held 99.9% uptime, but at 40°C, still within the claimed operating range, edge transaction errors tripled. These hidden limits meant the supplier's production-ready claim required substantial qualification before any rollout decision.
FAQ
Look for direct engineering involvement, proven coating uniformity data, and willingness to run sample trials on your actual fluid. A supplier that asks about viscosity, solids content, and target film thickness before quoting is usually more reliable than one that ships a standard catalog part.
Droplet size controls overspray, edge definition, and coating smoothness. With ultrasonic nozzles, median diameters often land between 13 and 40 microns depending on frequency. For thin conformal coatings, smaller droplets reduce pinholes; for fluxing or humidification, a slightly larger droplet can improve transfer efficiency.
A single nozzle can handle a range if the orifice and frequency are chosen correctly. Low-viscosity solvents, water-based coatings, and even some nanoparticle suspensions may work with the same body, but abrasive or high-solids fluids usually require a dedicated setup and possibly a different tip material.
Ask how the nozzle handles particle sizes close to the orifice diameter and whether the liquid path is easily flushed. Suppliers who offer a clear cleaning protocol, replaceable tip assemblies, and realistic recommendations for inline filtration tend to prevent most field failures.
The spray plume can appear stable while the actual film thickness varies due to fluctuations in liquid delivery pressure or electrical drive. A good supplier will help you integrate a closed-loop flow controller or at least validate repeatability with a gravimetric check, rather than relying on visual inspection alone.
Titanium bodies and PEEK or ceramic tips handle many solvents and mild acids, but highly alkaline or halogenated fluids may demand stainless steel or specialized coatings. Matching the wetted path to your chemistry prevents erosion, contamination, and drift in spray pattern after a few hundred hours.
If your current line has stable motion and liquid delivery, replacing nozzles can work. But most precision coating problems come from mismatched drivers, pulsation in the pump, or poor alignment. A supplier that offers a compact bench top or pilot system lets you validate the full setup before scaling, which often saves time and material.
Conclusion
Selecting an ultrasonic nozzle supplier means paying attention to details that rarely show up on a basic datasheet. Nozzle orifice geometry is a primary driver of coating edge quality; a sharp-edged orifice behaves very differently from a rounded or chamfered profile when the mist settles at the perimeter of a substrate. Frequency selection matters far beyond the droplet size chart. Higher frequencies deliver less mechanical energy to the film, which can be useful for heat-sensitive fluids, while lower frequencies push more kinetic energy into the surface and may improve wetting on difficult materials. Material compatibility should be evaluated across the entire flow path and adjacent components—seals, O-rings, fittings, and even the cleaning solvents used between batches can degrade parts that never contact the coating itself.
Spray angle variability is another factor that quietly undermines thin-film uniformity. Two nozzles with the same nominal angle can produce measurably different overlap patterns under real production conditions, leading to streaks or edge buildup that only appear after drying. Maintenance costs are frequently omitted from supplier quotes: replacing a piezoelectric transducer, recovering from a clogged orifice, or recalibrating after a cleaning cycle can outpace the initial capital cost over a year of continuous use. This is why supplier application testing deserves more weight than specification sheets. A proper trial with your actual fluid, substrate speed, and drying profile will expose hidden performance limits—such as viscosity ceilings, intermittent spray stability, or accelerated wear from abrasive particles—that no static catalog can predict.
Contact Us
Contact Person: Ivy Zhang
Email: [email protected]
Tel/WhatsApp: +86 1081502288
Website: https://www.siansonic.com/