Sanitary Ware Vertical Lift Plating Equipment: Efficient Finishing Solutions for Modern Manufacturing
2026-10-28
Every sanitary ware manufacturer knows the struggle: traditional plating lines take up too much floor space, drag turnaround times, and struggle to maintain consistent coating quality on complex ceramic shapes. As demand for flawless chrome and nickel finishes grows, many factories are hitting a wall with outdated horizontal processes. Vertical lift plating equipment changes that equation entirely—lifting workpieces through each stage reduces footprint, speeds throughput, and delivers uniform results that horizontal systems simply can't match. At the forefront of this shift is Junda, whose vertical lift systems are redefining what efficient finishing looks like in modern manufacturing. In this post, we'll break down how this technology works, why it outperforms conventional methods, and what to consider before upgrading your line.
Why Vertical Lift Systems Suit Sanitary Ware Lines
Sanitary ware lines rarely follow a straight path from casting to kiln. Pieces need to move between floor levels, cross drying zones, or queue for glazing without adding manual handling risks. A vertical lift system slots into that reality by using overhead space that horizontal conveyors simply cannot touch. Instead of sprawling across the shop floor, the lift carries basins or toilet bowls upward, downward, or to an elevated transfer point, leaving more room for operators and maintenance access. The compact footprint alone often justifies the investment in plants where square footage is already tight.
Another reason lift systems fit this segment is the way they handle fragile, high-value products. Ceramic bodies are heavy yet brittle, especially before firing. Vertical lifts with controlled acceleration and soft-stop positions reduce the jolts that cause hairline cracks or edge chipping. When a lift is paired with a simple pusher or robotic arm, fully automatic loading and unloading become practical without complicated conveyor routing. This allows a single lift to serve multiple stations—glazing, inspection, or packaging—so the line can be reconfigured as product mix changes, rather than being locked into a fixed path.
Getting Consistent Plating Thickness on Complex Shapes
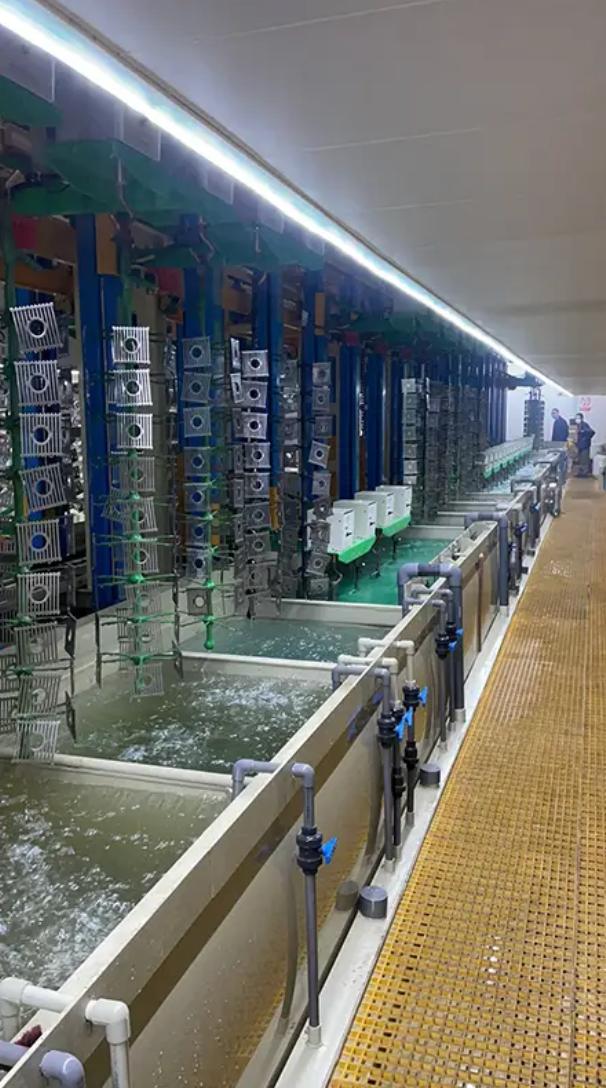
Achieving uniform plating on parts with recesses, sharp edges, or high-aspect-ratio features often comes down to current density management. On a flat panel, current distributes evenly, but once geometry changes, the field concentrates at outer corners and leaves inner pockets starved. Practical fixes include using conforming anodes or auxiliary anodes placed near recessed zones, plus pulse plating to let depleted ions recover before the next deposition cycle.
Fixture design also plays an outsized role. Rotating or oscillating the workpiece during plating helps break up the stagnant boundary layer that traps depleted solution in cavities. For deep holes or blind vias, forced solution flow through the feature is often more effective than increasing bath agitation alone. Small adjustments to rack positioning can shift the primary current distribution enough to flatten thickness variation by a visible margin.
Finally, bath chemistry can compensate for stubborn geometry. Levelers and brighteners alter polarization at high-current sites, slowing deposition where the field is strongest. Combining these additives with a lower average current density usually improves throwing power, though it increases process time. The trade-off is worth testing on a scrap part first—what works on a test coupon rarely translates directly to production tooling.
Streamlining Loading and Unloading Without Extra Labor
The quickest way to cut loading time isn’t adding hands—it’s removing the small delays that stack up at the dock. A set of aluminum dock boards left in place overnight, a pallet jack parked within arm’s reach, and a clearly taped staging grid let one worker roll a full pallet from trailer to bay without waiting for help or hunting for equipment. When every step has a reason and every tool has a home, the same crew finishes earlier.
Rethinking the flow from truck to shelf makes a bigger difference than most managers expect. Cross-docking inbound cartons straight to outbound lanes, or at least pre-sorting by route right at the trailer door, replaces double handling with a single scan-and-slide motion. The worker doesn’t lift more—they just stop lifting the same box twice.
Small mechanical upgrades pay for themselves in weeks. A used gravity conveyor along the dock edge, a lift table set at waist height, or spring-loaded dock levelers that match trailer height automatically all let momentum do the work. Pair those with staggered delivery windows so trucks aren’t stacked three deep, and the bottleneck disappears without hiring a single extra person.
Cutting Downtime with Modular Tank Layouts
When a single large tank needs cleaning, lining replacement, or an internal inspection, the usual response is to stop the process, drain the vessel, and lose production hours. Modular tank layouts change that calculation by splitting capacity across several smaller, independently valved units. Each module can be isolated from the rest of the system, so maintenance crews work on one section while the remaining tanks continue to feed the line. The result is less scheduled downtime, fewer emergency shutdowns, and the ability to spread maintenance across quieter periods instead of forcing a full stop.
Expansion and reconfiguration rarely require cutting into existing pipework or waiting for a new welded tank to be fabricated on site. Prefabricated modules with standardized flanges and baseplates connect to existing manifolds in hours rather than weeks. That means a plant can add storage capacity, change product grades, or reroute flows without taking the entire tank farm offline. Operators often find that the true savings come not from the equipment itself, but from avoiding the long coordination windows and permitting delays tied to major tie-ins.
On top of that, modular layouts pair well with automated valves and level sensors. A control system can shift load from a module nearing its maintenance interval to a standby unit without manual intervention. Crews then service the offline module at normal working pace, while production continues. Over time, what used to be a yearly shutdown becomes a series of small, low-risk changeovers, and downtime shifts from a costly event to a routine, almost invisible part of operations.
Smart Controls That Keep Bath Chemistry Stable
Modern plating lines often drift because operators rely on manual titrations and fixed addition schedules, which miss shifts in drag-out rates or anode efficiency. Smart controllers step in by reading actual bath activity every few minutes—monitoring amp-hours, pH, temperature, and even colorimetric brightener uptake—then adjusting metering pumps in small increments rather than dumping a full correction at once.
What separates a true smart system from a simple timer is its ability to learn from the line's rhythm. For example, a controller can anticipate higher nickel consumption during long barrel runs and pre-stage the next dose before concentration dips below the working window. It also logs the lag between addition and response, so if a bath tends to overshoot after a brightener shot, the software automatically trims the next pulse.
The result is less sawtooth chemistry, fewer rejected parts from dull or burned deposits, and a longer interval between bath dumps. Operators still make final decisions, but they get trend graphs and out-of-range alerts instead of guessing from a single grab sample.
Scaling Output While Keeping Finish Quality Tight
Ramping up production often tempts shops to loosen tolerances or accept rougher surface finishes as an unavoidable trade-off. But that compromise isn't a law of physics—it's a sign the process hasn't been examined closely enough. The trick lies in separating finishing from bulk material removal. When you push feed rates and depths of cut aggressively for roughing, you leave less stock for the final pass, but that final pass must stay precisely controlled. Many machinists unknowingly let the roughing strategy bleed into the finish pass, creating chatter marks or inconsistent Ra values across a batch. Instead, treat the finish pass as a separate, fixed constant: same tool engagement, same spindle speed, same coolant pressure, regardless of how many parts you're running per hour.
Another layer is tool wear monitoring tied to output volume. A finishing insert that looks fine at fifty parts might degrade noticeably by two hundred, even if the macro geometry still cuts. High-volume runs benefit from scheduled insert rotation based on measured surface data, not just visual inspection. Using a profilometer on every tenth part—or integrating an in-machine surface probe—catches drift before it turns into scrap. This isn't about spending more on tooling; it's about replacing guesswork with a predictable wear curve. When you know exactly how many parts a given edge can finish within spec, you can scale output without gambling on quality.
Finally, reconsider your workholding and thermal stability as volume climbs. Fixture clamping forces that work for a one-off prototype may distort thin walls or shift under rapid cycle times, producing finish variation that has nothing to do with the cutting parameters. Adding a second setup or switching to hydraulic clamping with lower, consistent pressure can keep the workpiece rigid without introducing stress. Similarly, spindle growth during long unattended runs changes the effective tool offset, subtly altering the depth of the finish pass. Compensating for thermal drift—either through warm-up cycles or real-time offset adjustments—keeps the finish tight even when the machine runs for ten hours straight. The goal is to make scaling output feel boring, because the finish quality never becomes a variable.
FAQ
Sanitary parts often have large, curved surfaces and intricate internal passages. Barrel plating tends to nest and scratch these pieces, while fixed rack plating limits access to recessed areas. A vertical lift system carries each rack straight up and down through the process tanks, so workpieces keep a consistent orientation and spacing. That reduces contact damage, allows higher current densities without burning, and suits the mix of sizes typical in faucet and shower hardware production.
The controlled up-and-down movement creates a gentle pumping action that pushes fresh electrolyte into cavities and threads. Because the part isn't static, the diffusion layer thins out, so metal ions reach low-current-density areas more readily. This helps avoid dull or thin deposits inside spout bores and behind flanges, which are common failure points on decorative chrome finishes.
Most lines are configured for multi-layer nickel-chrome systems: semi-bright nickel, bright nickel, microporous or microcracked nickel, then hexavalent or trivalent chrome. Beyond that, satin or brushed nickel, black chrome, antique bronze, and brass or copper undercoats are possible by adding extra plating tanks or post-treatment steps. The vertical lift design makes it easier to insert additional stations without major layout changes because the line is linear with shared automation.
Brass and zinc alloy parts go through different cleaning and activation steps than ABS plastic. A well-designed vertical lift line uses recipe-driven hoists: operators select the substrate program, and the system adjusts dwell times, lift speeds, and rectifier profiles automatically. For plastics, electroless nickel or copper is usually applied first to make the surface conductive, then the same decorative nickel-chrome sequence follows. Keeping dedicated pretreatment tanks for each substrate family prevents cross-contamination.
Throughput depends on rack density, part weight, and total plating time. A mid-size automatic line running a 60–90 minute nickel-chrome cycle might process 8–15 racks per hour if the hoist can transfer every 4–6 minutes. With 40–80 small parts per rack, that translates to roughly 300–1,200 pieces per hour. Larger shower valves or bath spouts will lower that number, but the vertical layout allows parallel flight bars to keep cycle times short.
The biggest issues are usually mechanical wear on the lift drive and contamination of the electrolyte. Regularly check chain or belt tension, guide rail alignment, and hoist limit switches; clean copper busbar contacts to prevent voltage drops; and filter or treat baths on schedule. Also watch for crust build-up on tank rims and lift arms, as dried salts can fall back into the bath and cause roughness. A weekly inspection of rectifier cooling fans and cables catches many electrical faults before they stop production.
Yes, integration is straightforward if planned early. The line can include counterflow rinses, drain boards, and collection trays that segregate rinse waters for treatment. Exhaust ducts with adjustable dampers connect to the plant's central scrubber system, and hoods over chrome and acid tanks capture fumes at the source. Some systems also add conductivity-controlled rinse water valves to reduce water use before it reaches the treatment plant.
Modern installations typically include hoist anti-collision sensors, tank-level alarms for heating elements, temperature interlocks, and emergency stop circuits along the operator side. Fume extraction interlocks prevent plating from starting if ventilation fails, and rectifier overload protection shuts down individual stations. For trivalent or hexavalent chrome tanks, enclosed process cells with automatic lid operation are becoming standard to reduce operator exposure.
Conclusion
Vertical lift plating lines address the stubborn challenges found in sanitary ware finishing by moving workpieces through a sequence of baths with precise, repeatable strokes. Unlike barrel or random-rack methods, the vertical travel keeps each part oriented for optimal drainage and current distribution, which is critical when faucet bodies, shower heads, and traps have deep recesses and hidden cavities. The controls allow operators to set ramp speeds, dwell times, and withdrawal angles independently for each station, so complex shapes receive a uniform deposit without burning edges or starving low-current areas. Loading and unloading become less labor-intensive because the lift arms return to a fixed ergonomic height, and jigs can be designed to grip multiple pieces without masking delicate threads or sealing faces.
Modular tank layouts cut downtime by letting maintenance crews isolate a single cell for cleaning or anode replacement while the rest of the line keeps running. Smart dosing systems continuously sample the electrolyte and make small chemical additions based on actual amp-hour totals rather than fixed timers, which keeps bath composition tighter and reduces sludge formation. This matters when a plant wants to scale output; the same vertical lift framework can be extended with additional stations without sacrificing finish quality. Real-time current monitoring flags drift before it becomes visible on the part, and automatic rectifier adjustments maintain consistent thickness across high-volume runs. The result is a sanitary ware finishing process that handles intricate geometries, lowers manual handling, and holds a stable, bright deposit from first piece to last.
Contact Us
Contact Person: hayyr
Email: [email protected]
Tel/WhatsApp: 8613082110525
Website: https://www.jundaelectroplating.com