Reliable INNOMOTICS Medium and High Voltage Frequency Inverters Manufacturer for Robust Industrial Drive Systems
2026-09-04
Medium and high voltage drive systems don't get second chances. A single inverter failure can halt an entire production line—and that's a risk no serious operation can afford. Chuangjuman has built its reputation as a manufacturer of reliable INNOMOTICS frequency inverters that keep industrial drive systems running strong under the toughest loads. Here's what sets their approach apart from the rest.
Where Standard Drives Fall Short, INNOMOTICS Steps Up
Standard drives are built around broad assumptions: predictable loads, moderate ambient conditions, and duty cycles that rarely push components to their edges. Real production floors rarely work that way. When a drive meets sudden torque reversals, sustained overload, or dust and vibration that creep past generic enclosures, the gap between datasheet and daily reality becomes painfully clear. INNOMOTICS closes that gap by designing from the application backwards, not from a generic platform forwards.
In heavy-duty conveying, mixing, or positioning tasks, a standard drive often forces engineers to oversize, add external braking, or accept nuisance trips that erode uptime. INNOMOTICS drives integrate heavier thermal margins, more robust power stages, and motion control features that handle those awkward in-between loads without extra hardware. The result is less cabinet clutter and fewer workarounds on the plant floor.
Where standard products treat challenging environments as exceptions, INNOMOTICS treats them as the starting point. Coated boards, reinforced terminals, and firmware tuned for real acceleration and deceleration profiles mean the drive keeps working when others derate or shut down. It is not about chasing spec-sheet extremes; it is about making sure the drive never becomes the reason a line stops.
Medium and High Voltage Inverters Built for Brutal Industrial Environments
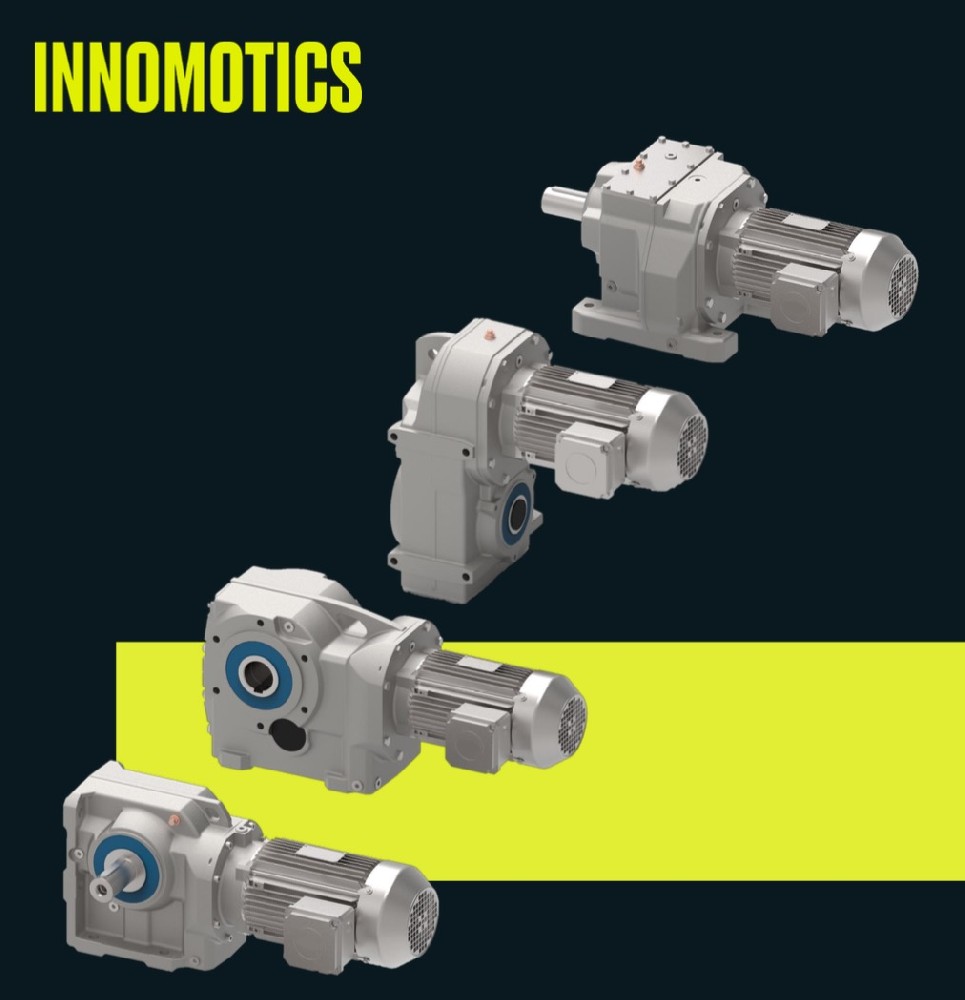
Industrial power conversion rarely happens in clean, climate-controlled rooms. Medium and high voltage inverters end up in places where dust coats everything, humidity spikes without warning, and vibration from nearby machinery is constant. The designs that survive here share a common trait: they assume the worst from day one. Thick powder-coated steel enclosures resist corrosion, while internal busbars and connectors are spaced and insulated to handle voltage stress even when airborne contaminants are present. Conformal coatings on PCBs prevent moisture and conductive dust from creating short circuits, and gasketed doors keep the worst of the environment outside where it belongs.
Thermal management is where many inverters fall short, especially when ambient temperatures swing from freezing nights to scorching afternoons. For medium and high voltage units, passive cooling alone is rarely enough. Instead, redundant fans or liquid cooling loops maintain safe junction temperatures without pulling contaminated air across sensitive components. Some designs use sealed air-to-air heat exchangers, so the internal air never mixes with the outside atmosphere. That matters in cement plants, mining operations, and offshore platforms where salt spray and conductive dust would otherwise coat heatsinks and degrade performance within months.
Maintenance also has to be realistic in these settings. No one wants to wait for a specialized technician to fly in just to swap a filter. Modular power cell designs let plant electricians replace a failed section quickly, often with the system still under partial load. Components are front-accessible, clearly labeled, and protected against arc flash. The goal is not just surviving the environment, but staying serviceable in it. That combination of rugged construction, aggressive thermal control, and practical serviceability is what separates an inverter that lasts a decade from one that becomes a recurring headache.
Reliability Is Engineered, Not Promised: Inside the Drive Design
Reliability in a drive starts long before the first spin-up. It lives in the bearing preload calculations, the tolerance stack on the rotor shaft, and the decision to run an angular contact pair instead of a deep groove ball bearing. A drive that simply meets its rated torque on a test bench hasn't proven much. The difference shows up in how the housing manages thermal growth, how the oil flings off the gear teeth at 9,000 rpm, and whether the seal lips stay cool enough to avoid hardening over a decade of stop-start cycles.
On the development side, the unglamorous work matters most: accelerated life tests at elevated ambient temperatures, torque ripple measurements under partial load, and strip-down inspections after thermal shock cycling. Designers who skip the metallurgy review or accept a slightly rougher gear flank finish will see failures that no warranty wording can paper over. The drives that earn a reputation for reliability are the ones where every snap ring, shim, and clearance was argued over in a design review, not added as an afterthought.
That is why field data from early prototypes is fed back into the next revision without waiting for a recall. A drive design only becomes trustworthy when the engineers treat a single fretting mark on a spline as a design flaw, not a routine wear pattern. Reliability, in this sense, is not promised in a brochure. It is machined, measured, and verified long before the product gets a nameplate.
Keeping Critical Processes Moving When Power Quality Gets Ugly
Industrial plants often run into voltage sags, harmonic distortion, or momentary interruptions that would knock lesser equipment offline. The trick isn't just having backup power standing by; it's designing control systems that tolerate messy waveforms without dropping a single scan cycle. A sag down to 70% nominal for three cycles might be invisible to a well-tuned drive, but it can scramble a PLC's I/O if the power supply isn't stiff enough. That's why critical loops get their own conditioned feeds and why every power-related alarm is tied to a graceful state hold rather than a hard stop.
Field experience shows that most unplanned downtime blamed on “the grid” actually traces back to poor ride-through settings or undersized DC bus capacitance. When the incoming line gets ugly, the first line of defense is often a simple sag corrector or an online UPS sized for only the logic side, not the whole motor load. This keeps the brain alive while the muscle rides out the disturbance. Some facilities take it further with dynamic voltage restorers on the main feeder, letting entire production lines coast through brownouts that would have caused hours of restart headaches.
The real payoff comes from testing everything under distorted conditions before it matters. A bench test with a programmable AC source can reveal that a seemingly robust panel will fault out at 85% voltage with 8% THD, while another configuration barely blinks. Documenting those limits lets you set protective relays and control logic to match reality instead of a spec sheet. When power gets genuinely hostile, the processes that keep moving are the ones that were never asked to be perfect—just stubborn enough to hold their state and wait for the sine wave to come back.
The Hidden Costs of Choosing the Wrong Frequency Inverter Manufacturer
The upfront price difference between inverter suppliers often masks bigger expenses that show up only after installation. A drive that fails early or trips unexpectedly can idle an entire production line, turning a saved few hundred dollars into thousands in lost output, overtime labor, and rushed replacement freight.
Mismatched support and sparse documentation quietly drain your maintenance budget. Your team may spend hours on the phone or reverse-engineering parameter settings because the manual lacks clear fault codes. Some low-cost units also stop receiving firmware updates, so a drive bought three years ago may not communicate with newer PLCs or safety systems, forcing an unplanned retrofit that eats the initial savings.
Then there is the inventory burden. If the manufacturer changes models frequently or exits a market, you are left stocking extra spares or replacing entire panels because one component is no longer available. These hidden costs never appear on the quote, but they compound over the drive's life and make the cheapest option the most expensive one.
From Conveyor Belts to Compressors: Real-World Drive Performance
When a conveyor belt grinds to a halt unplanned, it isn't just a mechanical failure—it's a breach of trust with the production schedule. The drive behind it, often a compact AC induction motor paired with a gearbox, works in an environment where dust, vibration, and constant load shifts are the norm. Real-world performance here means surviving the third shift on a Friday night when maintenance is already stretched thin. It's the difference between a bearing that whispers quietly for six months and one that screams for attention within weeks.
Move over to a screw compressor installation, and the demands change dramatically. The drive no longer just starts and stops a belt; it modulates speed to match air demand, often running 24/7 in a hot, oily enclosure. Inverter-duty motors with reinforced insulation and encoder feedback become non-negotiable if you want to avoid nuisance trips or premature winding failures. A drive that excels on a conveyor may struggle here unless it's designed for low-speed torque accuracy and thermal endurance—two traits that separate a true industrial workhorse from a paper spec sheet champion.
What ties these applications together is the unglamorous reality of performance: it's not peak efficiency on day one, but consistent behavior under real-world abuse. A drive that holds its current draw steady as a conveyor jams, or a compressor drive that doesn't fault when line voltage dips 10% on a hot afternoon—that's what operators remember. It's the reason some facilities standardize on one brand after years of trial and error, while others chase the lowest bid and pay for it in downtime.
FAQ
These inverters are built with robust power electronics and advanced cooling systems that handle continuous high-current operation. They also include protective features against voltage spikes and overloads, which keeps production lines running even in demanding settings.
The company uses proven semiconductor technology and performs extensive thermal and electrical stress testing before shipping. Redundant control options and built-in diagnostic tools further reduce the chance of unexpected downtime.
You'll find them in mining conveyors, cement mills, steel rolling lines, large pumps, and compressors. Anywhere a high-power motor needs precise speed control and long service life, these drives tend to be a practical choice.
Yes, the inverters support common industrial communication protocols and can be adapted to older switchgear. INNOMOTICS also provides commissioning assistance to make the transition smoother without major redesign.
The product range spans medium voltage drives from roughly 2.3 kV up to 13.8 kV, with power outputs reaching several tens of megawatts. This allows one manufacturer to cover everything from a single large fan to a whole processing line.
By adjusting motor speed to actual load requirements instead of running at fixed speed, they cut wasted energy significantly. Regenerative variants can even feed braking energy back into the grid, which improves overall system efficiency.
There is a global service network offering remote monitoring, spare parts, and on-site repair. The team also provides training for maintenance staff, which helps identify small issues before they become costly failures.
The main reasons are a long track record in medium and high voltage drives, strong engineering support during project planning, and lower total cost of ownership thanks to durable components and efficient service intervals.
Conclusion
Standard drives often stumble when faced with voltage sags, harmonic distortion, or the relentless heat and dust of heavy industry. INNOMOTICS medium and high voltage frequency inverters are built for exactly those conditions, not as an afterthought but as the core design brief. Instead of relying on promised specs, the engineering team hardens every stage—from DC bus capacitors to cooling architecture—so that a drive keeps a conveyor belt or compressor line moving even when incoming power quality gets ugly. That kind of toughness is what separates a true industrial partner from a commodity supplier.
Choosing the wrong manufacturer can quietly bleed a plant through unplanned downtime, frequent spare parts replacement, and derated operation. The real-world performance across conveyors, compressors, pumps, and fans shows that INNOMOTICS drives are sized and tested for brutal environments rather than idealized lab conditions. Where standard drives fall short, these inverters step up by maintaining torque stability and thermal headroom in continuous duty. The result is predictable uptime, lower lifetime cost, and a drive platform that earns its place in critical processes rather than simply occupying cabinet space.
Contact Us
Contact Person: Jony
Email: [email protected]
Tel/WhatsApp: 086-0571-86161808
Website: https://en.hzcjm.com/