Motorized Regulating Valve Manufacturer Selection Tips for Reliable Automation
2026-11-21
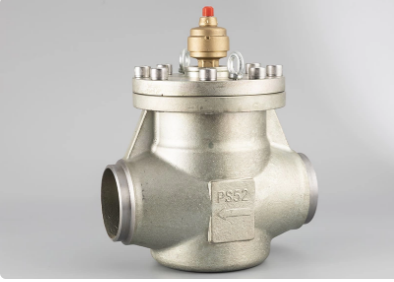
Selecting a motorized regulating valve often feels like choosing between nearly identical datasheets—until a field failure reminds you that control precision, response repeatability, and long-term reliability are not just spec sheet promises. For automation engineers, the difference usually lies in how the valve handles partial loads, fluctuating differential pressure, and constant cycling. That is where HONGSEN has focused its engineering effort: building motorized regulating valves that hold their setpoint without hunting, overcorrecting, or demanding frequent recalibration. In this guide, we look beyond the basic size and voltage selection and get into the practical manufacturer criteria that decide whether your automation loop stays stable or becomes a maintenance headache.
Look Past the Datasheet Accuracy Claim
That headline number on the front page usually comes from a carefully controlled bench setup, not from the messy reality of your board. Temperature drift, supply noise, input bias currents, and even humidity can quietly push a part well outside its advertised error band. The printed accuracy figure is often a best-case snapshot, not a promise that survives contact with a real circuit.
A far better habit is to read the conditions attached to the number. Check the fine print for test temperature, warm-up time, calibration interval, and whether the figure is a typical or a maximum value. Components age, references drift, and solder joints introduce thermal EMFs that no datasheet headline accounts for. If the specification only holds at 25 degrees Celsius with a stable supply and no load variation, it says very little about performance in the field.
The practical move is to treat the datasheet as a starting point for your own error budget. Measure the part in your actual layout, with your own grounding scheme and under the load conditions that matter for the application. A morning spent characterizing drift over temperature and supply range will tell you more than any glossy first-page accuracy claim ever will.
Match Positioner Dead Band to Your Loop
Dead band isn't a set-and-forget value—it should mirror how your loop actually behaves. If the loop tends to hunt or overshoot under small setpoint changes, tightening the dead band can make the positioner respond sooner, reducing wasted movement. But going too tight on a noisy process invites constant small corrections that wear out the valve stem and packing.
Start by watching the positioner's response to a 1–2% input change. If the valve barely moves or reacts late, widen the dead band slightly until the movement becomes intentional rather than jumpy. On loops with high static friction or older actuators, a slightly wider dead band often stabilizes control without sacrificing accuracy—especially when the process variable rarely needs fine positioning.
Match the dead band to the loop's natural rhythm, not a textbook default. For fast flow loops, keep it narrow to catch small deviations early. For slow level or temperature loops, a broader dead band prevents constant valve dithering. Test after each adjustment under normal operating conditions, and let the loop's own response tell you when the setting feels right.
Ask About Throttling Stability Near the Closed Position
Throttling stability rarely gets the attention it deserves until a valve is asked to hold a setpoint just off the seat. At small lifts, the relationship between stem movement and flow change is extremely steep, so a few thousandths of an inch can swing the flow coefficient by a wide margin. That nonlinear gain makes the loop prone to hunting, especially when the positioner overshoots and the plug repeatedly kisses the seat ring. Instead of chasing loop tuning alone, it is worth checking whether the trim has been characterized for that low-lift band and whether the actuator can resolve the small step changes being requested.
Fluid behavior near the closed position also changes in ways that show up as instability. A narrow annular gap produces high velocities, which can lead to localized flashing, cavitation, or noise before the valve is even visibly open. These effects disturb the flow stream and make the apparent position-flow curve erratic. In many cases the fix is not more aggressive control action but a different trim style, hardened materials, or staged pressure reduction that keeps the throttling point from falling into the unstable band.
A useful line of questioning for a supplier or engineer is to ask for actual low-lift performance data rather than the standard full-range curves. Request cycle testing or flow measurements at 2%, 5%, and 10% travel, and ask how much reversal error or dead band the actuator adds in that range. If the answers stay vague, that is usually a signal that the valve will need to be oversized or relocated to avoid operating where throttling stability is hardest to maintain.
Clarify Power Failure and Spring Return Behavior
When supply power drops or disappears completely, the actuator’s reaction hinges on the presence of a spring-return cartridge. In a true spring-return unit, the loss of motor torque unlatches a preloaded spring that drives the output shaft toward a designated fail position, normally open or normally closed. That direction is set mechanically during assembly and is not something an operator can reverse from the control room.
The transition itself may involve more than a simple snap. Certain designs add a short delay or hydraulic damping to soften the return stroke and protect connected valves from pressure surges. Field wiring also changes the picture: if a control signal fails while the main motor supply stays live, the actuator can hold its last position rather than spring back. The exact behavior depends on which terminals lose voltage.
During commissioning, it is worth documenting the real failure mode instead of relying on assumptions. Note the required energized terminals, the measured stroke time from full travel on power loss, and whether the final rest position matches the safe position called for in the process design. Actuators without a spring-return feature will typically remain at the last commanded position, so a fail-safe requirement should be confirmed and tested under actual load.
Compare Actuator Duty Cycle with Real Production Rhythm
A duty cycle that looks fine on a specification sheet often falls apart when it meets the actual rhythm of a line. The actuator may be rated for 40% or 60% duty, but the real question is whether those on/off intervals align with the physical cadence of clamps, stops, and transfer stations. When the production beat shifts—because a downstream station slows or an operator pauses the cycle—the actuator rarely sees the clean, repeating pattern assumed during sizing.
Watching the real sequence usually reveals mismatches that static calculations miss. A cylinder that cycles every nine seconds on paper might actually rest for twenty seconds, then fire three times in quick succession during a fault recovery or a manual jog. That irregular load pattern changes heat buildup, seal wear, and coil stress in ways a steady-state duty rating cannot capture. Comparing the logged duty cycle against the line’s true takt time often shows that the actuator is either oversized for normal running or dangerously close to its thermal limit during bursts.
The useful comparison is not just average percentage over an hour, but the distribution of active and idle periods against the line’s own pulses. An actuator running at 35% duty may appear safe, yet if those active windows stack tightly at every fourth cycle, the local temperature rise can exceed what the average suggests. Aligning duty-cycle data with real production rhythm means evaluating worst-case clusters, not just aggregate load, and adjusting the actuator choice or cooling strategy around those observed spikes.
Check Local Spare Parts and Service Reach Early
A machine bought without a nearby parts shelf is just a very expensive paperweight waiting to happen. Before you sign anything, map out where the closest genuine spares actually sit right now, not where a distributor promises they might be next quarter. Call the local dealer and ask what they physically keep in stock for your specific model, because a warehouse three states away won't help at 2 a.m. when a seal fails and your whole line is down.
Service reach works the same way. A technician who needs a flight and a hotel room will burn two days before turning a single bolt, while a local crew that knows the roads and has worked on identical units can often show up the same afternoon. Ask for the names of the last three customers in your area who needed emergency repairs, then phone them yourself. You'll hear the real story about response times, not the brochure version.
Strong spare parts availability and a local service footprint also change how you should read a quote. A slightly higher upfront price may be the cheapest option once you factor in the cost of waiting idle for a courier package or a visiting engineer. Treat early checks on parts and labor as part of the purchase negotiation, not an afterthought, and you'll avoid the classic trap of owning equipment that runs beautifully until the first small breakdown leaves you stranded for a week.
FAQ
Ask whether they size the valve for the actual control range, not just the line size. A capable supplier will request your minimum and maximum flow, pressure drop, and fluid properties, then confirm the expected opening stays within roughly 15 to 85 percent of travel. If the quote only matches the pipe diameter, treat that as a warning sign.
Request the actuator's duty cycle, backlash, and positioning resolution. For continuous modulation you need a motor rated for frequent reversals, low mechanical play, and a positioner or onboard controller with a tight deadband. If the manufacturer cannot provide those details or simply labels the unit as suitable for both open/close and modulating service, keep evaluating.
Ask how the valve reacts to signal loss, which control inputs it accepts such as 0-10 V, 4-20 mA, Modbus, or BACnet, and what feedback outputs are available. A knowledgeable manufacturer will explain fail-safe behavior, position feedback options, and typical wiring without making you chase several departments.
Because motorized regulating valves sit inside control loops where small shifts in response can disrupt an entire process. Direct technical support, stocked spares, and clear calibration procedures help you resolve signal drift, actuator faults, or seal wear without long downtime. A low initial price often becomes irrelevant after one unresolved commissioning issue.
Look beyond the bare valve and actuator. Mounting hardware, linkage, positioners, feedback modules, calibration software, freight, and import duties can all appear as separate line items. Also confirm whether startup assistance and tuning support are included or billed separately.
Ask for test data covering hysteresis and repeatability, not just a single accuracy figure. A useful supplier can provide a curve showing stem position against input signal over multiple cycles. That reveals more about real-world control behavior than a headline number on a datasheet.
Body, trim, and seal materials have to match the fluid, pressure, and temperature conditions at the actual control point. A manufacturer that asks about corrosion, erosion, and temperature cycling before quoting is doing proper due diligence. If they offer one standard seal without asking about your media, the valve may test well but fail early in service.
When it drifts out of calibration, overshoots the setpoint, or fails during a batch and causes scrap, rework, or an unplanned shutdown. A low-cost actuator with coarse resolution can force the control loop to hunt, wearing out the valve and connected equipment. The real expense is the process instability it introduces, not the purchase order.
Conclusion
A reliable automated valve package rarely fails because of a single published specification. It fails when the stated accuracy only holds on a test bench, while the positioner dead band is too wide for the actual loop it has to control. Before comparing manufacturers, ask how the valve performs during small corrections near the closed position. Many units look stable at mid-stroke but hunt or slam once the plug approaches the seat. That narrow region often determines product quality, waste, and wear far more than the full-scale accuracy figure. Instead of relying on a datasheet claim, request factory data or a short video showing step changes at 2–5% opening under real loading conditions. If the maker cannot show repeatable, calm movement in that range, the quoted accuracy has little value in your process.
Power failure behavior matters as much as normal operation. Clarify whether the actuator fails in place, drives to a safe position, or uses a spring return, and ask how long that stroke takes under full differential pressure. Then compare the published duty cycle with your real production rhythm: frequent small corrections, continuous modulation, or hot ambient conditions can push a standard motor beyond its thermal limits even when the catalog suggests adequate capacity. Finally, check local spare parts and service reach early. A nearby partner holding common seals, boards, and motors in stock will keep a line running far better than a slightly cheaper valve tied to long international lead times. These practical factors usually decide whether the automation stays reliable after the initial installation.
Contact Us
Contact Person: KOPASS HO
Email: [email protected]
Tel/WhatsApp: 8613606566112
Website: https://www.hongsenref.com/