Good Quality Food Extruder Your Complete Selection Guide
2026-09-28
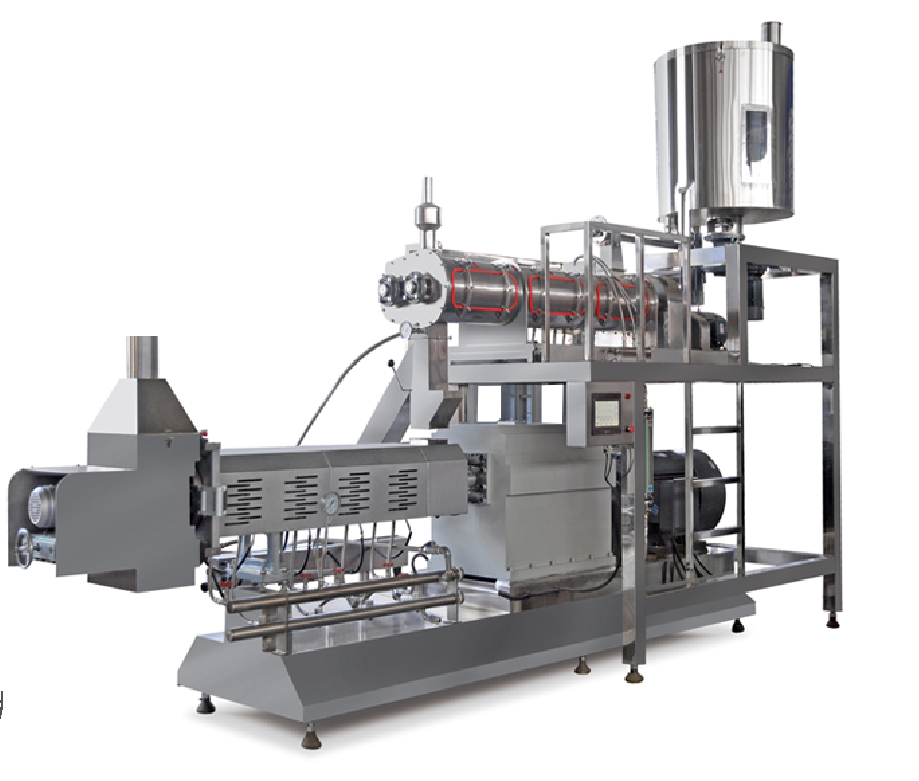
Choosing a food extruder can feel overwhelming—especially when every supplier claims their machine is 'the best.' But here’s the truth: quality isn’t just about shiny specs or low prices. It’s about consistency, durability, and how well the equipment adapts to your production goals. In this complete selection guide, we’ll walk you through the key factors that separate a reliable workhorse from a costly mistake. Whether you’re scaling up a snack line or venturing into textured proteins, knowing what to look for saves time, money, and headaches. And when it comes to trusted manufacturers, MINGDE has built a reputation for robust engineering and real-world performance. Ready to make an informed choice? Let’s dive into the details that matter.
What's Inside the Barrel Determines Whether You Make Product or Scrap
Every barrel tells a story before the machine even starts. Walk past a line of drums in any plastics or rubber shop and you'll see it: one barrel caked with degraded resin at the feed throat, another with a scorched zone near the metering section, and a third running clean. The difference isn't luck or operator mood. It's what gets poured in at the top. Fill a barrel with moisture-laden regrind, mixed-color flake, or resin that sat too long near a heat vent, and you've already written the ending. No screw design, no barrel temperature profile, no amount of purging compound can fully undo a bad material decision at the hopper.
Think of the barrel as a narrow, heated corridor with very little room for error. As material moves from the feed zone to the compression zone to the metering zone, it relies on predictable viscosity, consistent pellet size, and a tight melt temperature window. Toss in dust, fines, or a random chunk of cardboard from a gaylord, and the screw starts to slip, surge, or stall. The barrel doesn't care what the spec sheet says. It only reacts to what's physically inside. A single wet pellet can produce a gas bubble that turns into a burn mark two shots later. A stray metal shaving can score the barrel wall, and from that moment on, every subsequent product carries a scar you can't buff out.
So before you blame the press, the mold, or the technician, look at the raw material. Is the regrind percentage too high? Are you mixing lots with different melt flows? Has the virgin resin been stored next to a wash bay or a dusty grinder? These aren't trivial questions; they determine whether the barrel delivers good melt to the nozzle or becomes a scrap generator. Production managers who keep a log of material lot changes, moisture readings, and visual inspections at the hopper tend to sleep better. The ones who say "it's all just plastic" end up with barrels full of carbon and a mountain of rejected parts by Friday.
Materials and Welds That Separate Long-Run Machines from Frequent Failures
A machine that runs for years without a hitch rarely owes its longevity to luck. The difference often sits in the grain of the metal and the integrity of a joint hidden beneath paint. Operators who chase uptime learn to look past glossy spec sheets and ask harder questions about base alloys, heat treatment, and the quiet competence of a welder who understands fatigue.
Take the frame of a high-cycle stamping press. Some builders use rolled steel plate with a tensile strength near the bare minimum for the load rating. Others step up to a normalized fine-grain alloy that resists crack propagation long after the first million strokes. The weld procedure matters just as much as the material. A full-penetration groove weld with controlled interpass temperature produces a joint that flexes with the structure instead of fighting it. A quick fillet weld, laid too cold or too fast, can hide undercut and slag inclusions that become stress risers under repetitive shock.
In the field, the evidence is blunt. Machines built with ordinary mild steel and short-circuit MIG welds show fatigue cracks in the same corners year after year. Machines built with quenched-and-tempered plate and mechanized submerged arc welding run maintenance intervals that stretch from months to seasons. That gap is not marketing speak. It is the cumulative effect of choosing a better filler metal, controlling heat input, and refusing to let a bad weld pass just because it looks fine from the outside.
Why Screw Profiles and Barrel Liners Deserve More Attention
Most processors treat the screw and barrel as static workhorses — set them up once, run them for years, and only react when output drops or melt temperature spikes. That mindset quietly drains profit. The screw profile, specifically the depths, compression ratio, and mixing section geometry, determines how evenly material plasticates, how much shear heat is generated, and whether additives get dispersed or merely smeared. A mismatched profile can push energy costs up 15% or more while producing parts with inconsistent density or surface streaks, yet the problem often gets blamed on raw material variation.
Barrel liners receive even less scrutiny, partly because they are hidden inside a thick steel housing. However, the liner alloy and surface finish directly control wear life and the ability to maintain tight clearances with the screw flight. In abrasive or corrosive environments, a standard nitrided liner may wear unevenly, creating a barrel that is effectively conical after a few thousand hours. This forces the screw to work harder, generates more frictional heat, and eventually leads to black specks or degraded material in the melt. Swapping in a bimetallic liner with a harder bore surface often doubles service life without changing any other process parameter.
Paying attention to these components is not about chasing marginal gains — it is about avoiding the slow drift into higher scrap rates and unplanned downtime. A well-chosen screw profile and liner combination, reviewed against actual material and output targets, can reduce energy per kilogram, stabilize melt pressure, and extend maintenance intervals from months to years. When processors finally map their wear patterns and adjust geometries accordingly, the improvement is usually immediate and measurable, proving that these so-called commodity parts deserve a central role in process optimization.
Sanitary Design That Cleans Fast Enough for Your Shortest Changeover
Changeover speed often stalls at the washdown step, so we removed the places where product and cleaning fluid linger. Frame members are sloped 45 degrees instead of sitting flat, pipes are spaced to let a hand or spray wand pass between them, and belt lifts are tool-free, so there is no bolt hole collecting residue.
Every stainless contact surface has a continuous polished finish with no crevices or dead ends. Manifolds drain completely when the line stops, and hinged guards swing clear without removing fasteners. The result is not just a faster rinse, but fewer places for allergens or bacteria to hide between runs.
Reading Motor Power and Real Throughput Without the Marketing Hype
Wattage stickers on motors are almost useless for predicting real-world performance. A grinder labeled 400W can feel weaker than a 300W model if its power curve drops sharply under load or if the drive train wastes torque. The only honest way to compare is to measure actual current draw while the motor is working through your material, not just spinning freely. That number tells you how much work is being done at the burrs or blades, which is what actually matters.
Throughput is another spec that gets inflated. Many machines can hit an impressive grams-per-second figure for a short burst, then slow down as heat builds or the motor protection kicks in. Real throughput means the sustained rate over a full session, using the grind size and bean density you actually work with. If you cannot get that number from a spec sheet, run your own timed test with a scale and a stopwatch. Ignore the peak ratings.
Reading motor power and throughput without the hype comes down to watching for what is missing: continuous torque curves, duty cycle limits, and honest testing conditions. If a manufacturer only lists maximum watts or a one-second throughput, assume the real-world numbers are lower. Good machines earn their reputation through repeatable, measured output, not through cleverly framed marketing claims.
The True Cost of Ownership Starts After the Warranty Ends
Most buyers focus on the sticker price, the monthly payment, or the warranty terms when making a purchase. But the real financial story often begins the moment the manufacturer's warranty expires. A product that seemed affordable can quickly become a burden as out-of-pocket repair costs, replacement parts, and service fees start piling up. Without the safety net of a warranty, even a minor malfunction can turn into a significant expense, and the cumulative effect over the product's remaining lifespan can dwarf the original savings.
This is where true cost of ownership becomes critical. It's not just about what you pay upfront; it's about what you'll pay over the entire useful life of the item. A cheaper product with a short warranty might end up costing far more than a slightly pricier one with longer coverage or better build quality. Smart buyers look beyond the warranty's expiration date and factor in reliability data, replacement part costs, and the likelihood of failure after the guarantee ends.
Planning for post-warranty expenses is essential for both individuals and businesses. Setting aside a maintenance reserve, choosing products with modular designs that allow for inexpensive repairs, or simply knowing when to replace rather than repair can save thousands in the long run. The goal isn't just to survive the warranty period—it's to thrive well after it's over, without being blindsided by hidden costs.
FAQ
Focus on the barrel and screw material first—stainless steel or food-grade alloy resists wear and corrosion. Check the drive motor's continuous torque rating, not just peak power. Also look for precise temperature zones, easy disassembly for cleaning, and safety interlocks on the die head.
Calculate your hourly output target, then add a 20–30% buffer for growth and recipe variations. Don't size by motor power alone; ask the manufacturer for actual throughput data with a similar recipe. A slightly larger extruder running at 70–80% of its capacity usually lasts longer than one maxed out.
The barrel and screw should be made of nitrided steel or stainless steel with a hard chrome plating on wear surfaces. Look for a robust gearbox from a known supplier, sealed bearings, and a frame that doesn't flex under load. Cheap cast iron parts may save money upfront but lead to contamination and frequent replacements.
Many twin-screw extruders can switch between snacks, cereals, and pet food with screw profile changes and different die plates. Single-screw models are more limited. If you plan to run diverse recipes, choose a modular barrel and screw design so you can reconfigure rather than buy separate machines.
Screw geometry—flight depth, pitch, and mixing elements—controls shear, residence time, and pressure. High shear gives puffed, light textures; low shear produces dense, chewy products. Work with the supplier to match the screw profile to your target mouthfeel rather than accepting a one-size-fits-all setup.
It's critical. Too much heat denatures proteins and scorches sugars; too little prevents proper gelatinization. Look for independent heating and cooling zones along the barrel, accurate thermocouples, and a control system that can hold ±1–2°C. Manual dials are fine for simple products, but PLC-controlled zones give repeatable quality.
Worn screw elements and barrel liners are the most common, often caused by abrasive ingredients or running dry. Schedule regular inspections of clearances and replace wear parts before they affect product quality. Keep the die area clean to prevent blockages, and lubricate bearings according to the manual—not over-greasing.
For most small businesses, a twin-screw extruder offers more flexibility in ingredients, moisture, and product shape, though it costs more upfront. A single-screw is simpler, cheaper, and fine for a narrow product line like plain pellets or puffed snacks. Consider your product range and future expansion before deciding.
Conclusion
A good food extruder earns its reputation long before the first batch is run. The barrel interior dictates whether you are shaping saleable product or feeding the scrap bin, so look for finishes and clearances that keep material moving without dead spots. Equally telling are the materials and welds: machines built for long campaigns use frame and screw alloys that resist fatigue, with welds that do not become crack initiation sites after thermal cycling. Screw profiles and barrel liners often get overlooked because they are hidden from view, but they control shear, mixing, and wear life; a carefully matched profile and a properly specified liner separate a line that runs weekend after weekend from one that needs constant adjustment.
Sanitary design is not a marketing checkbox—it is the difference between a 20-minute changeover and a half-shift teardown. Pay attention to how easily the barrel and screw can be accessed, whether surfaces drain completely, and how many tools are needed to reach product contact areas. When evaluating performance, ignore the inflated motor ratings and ask for real throughput at actual moisture, temperature, and pressure conditions; a machine that draws less power for the same output is often the better engineered one. Finally, remember that the purchase price is only the entry fee. True cost of ownership shows up in spare parts, downtime, service response, and how many years the machine can hold tolerance before a rebuild—so choose based on what happens after the warranty, not what is printed on the brochure.
Contact Us
Contact Person: LILY SUN
Email: [email protected]
Tel/WhatsApp: 0086-13969103791
Website: https://www.snackfoodmachinery.com/