Elastic Band Exporter: Key Factors for Global Sourcing Success
2026-10-24
Sourcing elastic bands globally can be trickier than it looks—quality varies widely, lead times slip, and hidden costs pile up. Yet for importers and distributors, getting it right is the difference between repeat orders and returned shipments. That's where understanding the key factors—from material consistency to compliance—becomes essential. At YONGFENG, we've seen how these decisions shape supply chain resilience. In this post, we break down what truly matters when choosing an elastic band exporter, so you can source with confidence.
Material Choices That Withstand Repeated Stretch Without Losing Snap
When a garment or component is expected to endure frequent stretching, the raw material itself does most of the work. Elastane fibers such as Lycra or spandex blends remain popular because their molecular chains can elongate under tension and then recoil without permanent deformation. Yet pure elastane is rarely used alone; it is usually wrapped or plied with nylon, polyester, or cotton to add structure and prevent the rubbery feel that comes with high elastic content. For applications that demand both recovery and breathability, a nylon-spandex knit in the 15–20% elastane range tends to hold its silhouette through hundreds of wear cycles. Natural rubber latex is another strong candidate for bands and cords, though it can degrade with oils and UV exposure, so it is often reserved for protected interiors.
Beyond fibers, certain urethane films and silicone sheets offer an alternative route to lasting snap. Thermoplastic polyurethane, for instance, maintains a high elongation at break and springs back even after repeated extension, which makes it common in activewear trims, medical wraps, and stretch pouches. Silicone, while softer to the touch, resists compression set and remains elastic across a wide temperature range. If the product will be stretched many times a day, it is also wise to look at fabric construction: rib knits and interlock knits provide built-in mechanical stretch that complements the fiber's own recovery. Pairing a resilient yarn with a knit that does not fight the motion usually yields the best long-term performance.
Certification Hurdles That Separate Genuine Exporters from Amateurs
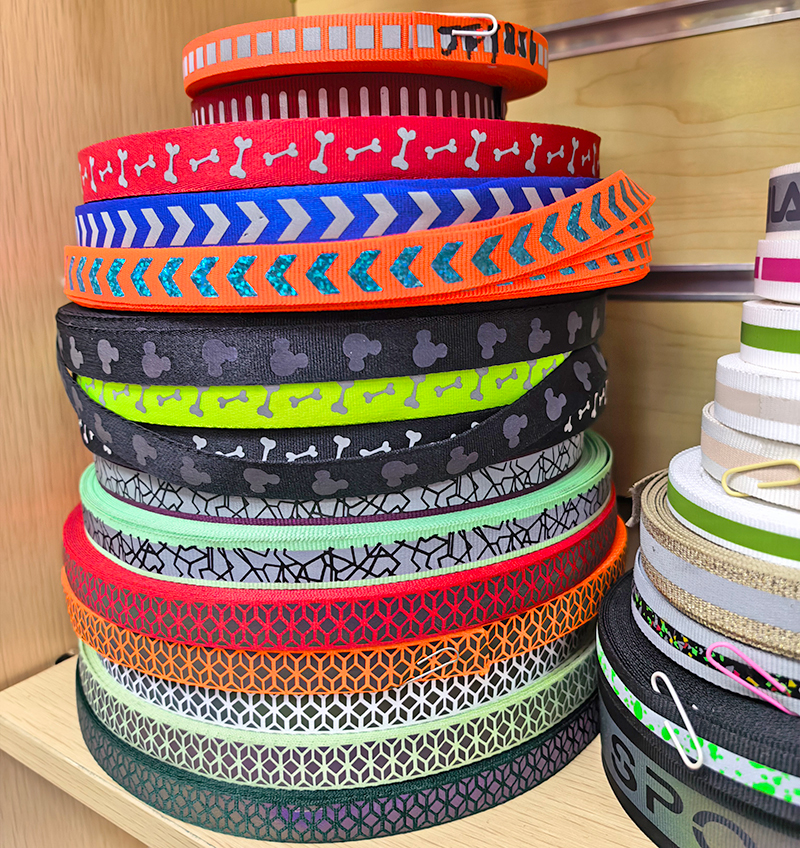
Genuine exporters treat certification as a fixed cost of entering a market, not an optional add-on. They budget for third-party audits, lab testing, and renewal fees before quoting a single client. Amateurs often set a price first, then discover that organic or electrical safety approval will take four months and cost more than the initial order.
The real separator shows up in traceability paperwork. A serious exporter can produce batch records, supplier declarations, and chain-of-custody documents within a day because they built the system before the certifier asked. Amateurs scramble, ask the buyer what documents are needed, or send a certificate that expired two years ago and hope nobody checks.
Another hurdle is handling standard conflicts between destination markets. A product certified for EU Organic may still fail Japanese JAS requirements, and a CE mark does not automatically satisfy GCC or UL expectations. Experienced exporters map these differences early and choose certifications that match their actual buyers, while amateurs collect marks without reading the scope or validity conditions.
Depth of Customization: Thread Counts, Weave Patterns, and Finishing Options
When you dig into customization, thread count isn't just a number—it's a spectrum. We work with counts as low as 144 for that airy, rumpled linen feel all the way up to 1,200 for an ultra-dense sateen that almost feels cool to the touch. But here's the nuance most people miss: a tight 300-count percale can feel crisper than a looser 600-count sateen, so we guide you through the trade-off between breathability, durability, and that silky drape you're after. We even blend different counts in the same fabric—say, a 400-count warp with a 250-count weft—to hit a specific weight and hand feel you can't get off the shelf.
Weave patterns go far beyond the basic percale and sateen split. You can choose a classic basket weave for a subtle grid texture, a herringbone twill that shifts under light, a waffle weave with actual thermal loft, or even a jacquard where the pattern is woven into the structure rather than printed on top. Want something truly unique? We can run a dobby loom to create small geometric repeats—think tiny diamonds or diagonal ribs—that add tactile interest without shouting. And if you're torn between two patterns, we can weave a reversible fabric: one side a smooth sateen, the other a matte twill, so you get two finishes in a single sheet.
Finishing options are where customization gets quietly transformative. A mercerization bath swells the cotton fibers, boosting sheen and dye uptake for richer colors. Enzyme washes soften the surface without the chemical stiffness of traditional softeners. Sanforization pre-shrinks the fabric so it won't distort after the first wash. But the real differentiator is a calender finish—we can run the fabric through heated rollers at different pressures to achieve anything from a barely-there smoothness to a polished, almost glassy surface. For those who hate ironing, a wrinkle-release finish is available, though we always note it trades a bit of natural crispness for convenience. Each finish shifts the hand feel, luster, and longevity, so we sample three variants before locking in your final choice.
Scaling Production While Keeping Tension Uniform Across Every Batch
Ramping a web line from pilot to full production usually exposes the hidden slack in your tension strategy. Narrow rolls tolerate a few pounds of drift; wide rolls don't. The fix isn't swapping in bigger drives. It's mapping where tension actually changes: during splices, core changes, ramp-up, and at the lay-on roller. Without that map, every speed increase just amplifies the same defects.
For batch-to-batch consistency, we run closed-loop tension control that references live roll diameter and measured web modulus. Each unwind, process, and rewind zone gets its own setpoint curve, with trim values that account for brake fade on older unwinds or nip hardness on the rewind. The result is a recipe that doesn't drift when a new operator takes over or when raw material arrives from a different lot.
Where this really shows is in roll hardness profiles. If tension control only reacts after deviation, the last 500 meters of a roll will feel different from the first. So we apply predictive offsets learned from previous torque curves before a new batch starts. That keeps edge quality and slitting registration stable even when the line runs 24 hours at 40 percent above its original rated speed.
Packaging Decisions That Guard Against Fraying and Moisture in Transit
When goods leave your facility, the real test begins on trucks, ships, and cargo holds where vibration, humidity shifts, and rough handling are daily realities. Choosing a barrier material is rarely as simple as picking the thickest film. A woven polypropylene sack might excel at resisting tears, but without a laminated liner its open weave lets moisture creep in through the seams. Many logistics teams overlook how thread type and stitch density interact with edge protection. A dense lockstitch along folded hems, combined with a strip of reinforced tape inside the seam allowance, keeps fibers from unraveling even when a carton is dragged across a dock plate.
Moisture defense starts long before the container is sealed. Desiccant packs placed only at the top of a carton leave the bottom layer vulnerable to condensation that pools during temperature swings. Instead, specifiers often opt for a full vapor-barrier liner with a water vapor transmission rate below 0.5 grams per 100 square inches per day, then seal corners with heat rather than adhesive tape. That heat seal removes the weak point where peel-and-stick tape can lift when exposed to humidity. For bulk shipments, a hood-style stretch film applied over the pallet can shed rain while still allowing trapped air to escape through micro-perforations, preventing a balloon effect that stresses the outer wrap.
Fraying is often dismissed as a cosmetic issue until a torn edge catches on a conveyor and splits an entire bag open. A simple upgrade is switching from a plain cut edge to a folded, glued hem on open-mouth bags. That single change shifts failure from the fabric itself to the adhesive bond, which can be tested with a peel fixture at 180 degrees. Pair it with an outer carton that has a water-resistant coating on the inside flaps, not the outside, so that any liquid that seeps through the corrugated outer layer is channeled away from the product instead of being absorbed. These are the kind of quiet decisions that prevent damage claims and keep customers from ever knowing what could have gone wrong.
Clear Communication Cadence That Prevents Specification Drift
Scope creep rarely announces itself with a formal request. It slips in through casual Slack threads, a stray comment in standup, or an innocent "while we're in there" during a code review. The most reliable guardrail isn't a better requirements doc—it's a predictable rhythm of check-ins where the team explicitly re-anchors to the original spec. When every Monday starts with a five-minute read-through of the core acceptance criteria, and every Friday ends with a diff comparison between what was built and what was originally written, deviations become visible before they calcify.
The trick is to make these touchpoints feel less like bureaucratic gates and more like breathing room. Instead of asking "are we on track?"—a question that invites optimistic hand-waving—ask "what did we learn this week that should change the spec?" That reframe gives people permission to surface drift without feeling like they're confessing to failure. Pair that with a shared living document that logs every proposed change with a one-line rationale, and you'll start to see patterns: the same module getting "clarified" three times, a stakeholder who only raises concerns after demos, or a feature that keeps absorbing adjacent requests because it was under-specified from the start.
Consistency matters more than intensity. A lightweight cadence—say, a fifteen-minute spec sync every Tuesday and Thursday—beats a monthly deep-dive because it shortens the gap between when drift happens and when it's caught. Team members stop treating the spec as a frozen artifact and start treating it as a living contract that gets renegotiated in small, deliberate increments. And when someone does propose a change, the default response becomes a calm "let's log it and size the impact before we commit," not a defensive "no, we already agreed." That shift in tone—from guarding the spec to governing it together—is what ultimately keeps a project from drifting into something nobody originally asked for.
FAQ
Focus on consistency in production, raw material sourcing, and quality checks. A reliable exporter typically maintains close relationships with rubber suppliers and uses standardized testing for elongation, tensile strength, and colorfastness before shipment.
Shorter lead times reduce inventory risk, but only if the exporter doesn't sacrifice quality. Buyers often weigh the exporter's ability to scale production during peak seasons against their historical on-time delivery rates.
Traceability helps confirm the rubber or synthetic blend meets safety and durability standards. It also simplifies compliance checks and reduces the chance of receiving batches with inconsistent stretch recovery.
Thoughtful packaging prevents tangling, moisture damage, and color transfer during transit. Exporters that use humidity-resistant wrapping and clearly labeled cartons save buyers time at distribution centers.
Request third-party inspection reports, batch samples, and video walkthroughs of production lines. A trustworthy exporter will also share rejection rates and corrective action plans from past orders.
Beyond unit price, buyers should watch for additional charges like customs brokerage, inland freight, repackaging due to damage, and rework caused by inconsistent band elasticity or thickness.
Flexible MOQs allow buyers to test new sizes and colors without overstocking. Exporters willing to adjust MOQs for repeat clients often signal stronger partnership commitment.
Clear, proactive updates on production milestones and potential delays. Exporters that confirm specifications in writing and ask clarifying questions before starting orders tend to avoid costly misunderstandings.
Conclusion
Start with the raw material. A band that loses its snap after a few wears isn't just a quality flaw—it's a failed shipment in the making. Exporters who consistently deliver work with a narrow set of tested rubber and spandex blends, checking elongation recovery before committing to a full run. But materials alone won't clear customs or win retail accounts. Genuine exporters carry the paperwork to prove it: OEKO-TEX, REACH, or regional equivalents showing no restricted dyes or heavy metals. Then comes the depth of customization. Thread counts, weave density, and edge finishing aren't afterthoughts for serious buyers; they're the baseline. A factory that tweaks warp and weft ratios without wrecking lead times is the one that keeps repeat orders flowing.
Scaling that precision is where many suppliers slip. Holding uniform tension across thousands of meters isn't luck—it's calibrated knitting machines and tension checks at several points along the roll, not just the start. Packaging matters just as much. Bands that arrive frayed or damp because they were loosely spooled or packed in thin poly bags can sour a relationship faster than a missed deadline. And without a clear communication rhythm—weekly photo updates, shared spec sheets with revision dates, and a single contact who actually reads the notes—specification drift creeps in. The best exporters treat sourcing as a continuous loop, not a one-time transaction. They flag shortages before they happen, confirm dyelot approvals in writing, and make it easy for a buyer to trust the next container before the current one has even cleared the port.
Contact Us
Contact Person: Mr Deng
Email: [email protected]
Tel/WhatsApp: +86-18926872657
Website: https://www.uniyongfeng.com/