China Hard Chrome Plating Equipment That Industrial Finishers Trust
2026-09-08
Plating lines fail in predictable ways—burning on edges, poor throw in recesses, tanks that leak heat and money. So when industrial finishers start ordering hard chrome plating equipment from China, they're not chasing the lowest bid. They're chasing a supplier that has already earned their trust. That supplier is increasingly Junda. What follows is a look at why shops that once insisted on European or American brands are now putting Junda's rectifiers, tanks, and automation at the center of their production.
Built for Shops That Can't Afford Downtime
Every time your store stutters, you're not just losing a sale—you're handing that customer to a competitor. Downtime during a flash sale, a product launch, or even a random Tuesday afternoon carries the same cost: trust evaporates and revenue follows. Shops that live on thin margins or rely on recurring orders need infrastructure that treats uptime as a baseline, not a bonus. That means auto-scaling during traffic spikes, redundant server clusters that fail over without a hiccup, and continuous health checks that catch issues before they become outages. The goal isn't to recover quickly; it's to never need recovery in the first place.
Think about the last time you refreshed a checkout page and watched it spin. That's the moment the sale dies. For high-volume stores, even 99.9% uptime translates to nearly nine hours of potential loss every year—and few shops can stomach that math. What you need is a backend that's been stress-tested under real buying surges, not just simulated traffic. Database replication across multiple regions, queue-based order processing, and a CDN that keeps product images and carts loading even when one node goes dark. When your payment gateway hiccups, the system should retry gracefully in the background, not dump the customer back to an empty cart. Uptime isn't a metric; it's the silent salesperson you never have to check on.
Where Thickness Tolerance Really Counts
You can spec a sheet of steel down to a few thousandths and still end up with a bracket that fights you on the assembly line. The places where thickness tolerance really matters aren't always the obvious ones. Think about a bearing seat that's been machined after forming—if the raw material came in thick, you cut away more, the part heats differently, and suddenly a dimension that was fine on paper drifts out of spec. Or consider stacked laminations in a motor core: a consistent thickness matters less than a predictable one, because compression and magnetic performance shift when one layer is slightly proud of its neighbor. What gets overlooked is how tolerance interacts with everything downstream—bending, welding, coating. A tight thickness range doesn't just make inspection easier; it keeps the next operation from inheriting someone else's variation.
That's why the real conversation about thickness tolerance should happen before the first prototype, not after a batch of parts gets rejected. If you're stamping a deep-drawn housing, the blank's thickness variation shows up as uneven wall thinning and can turn a cosmetic ripple into a stress riser. In roll forming, a material that's within tolerance but on the thin side might spring back differently, changing the profile angle just enough to cause fit-up problems at the weld station. Even in less demanding applications—brackets, covers, simple clips—thickness variation quietly affects torque specs for fasteners, because the joint's stiffness changes with material thickness. Ignoring that is like tuning an instrument without checking whether the strings are all the same gauge.
None of this means you need a narrower tolerance on every dimension. It means you need to identify the few places where thickness variation amplifies through the process. A good starting point is to trace what happens after the blank is cut: does it get coined, bent sharply, or welded to a different alloy? Each of those steps reacts differently to a few percent change in thickness. Then talk to the people running the press or the brake—they already know which coils cause trouble, because they feel it in reject rates and tool wear. Getting that feedback before you lock in a material spec is the difference between designing a part and designing a process that actually holds up when the mill delivers at the edge of its published range.
The China Sourcing Shift No One Talks About
While headlines fixate on factory relocations to Vietnam or Mexico, a quieter change is happening inside China itself. Sourcing managers are no longer chasing the absolute lowest unit cost. They're negotiating for continuity guarantees, local raw material access, and faster prototyping loops that make a 15% price gap less relevant than a two-week lead time reduction. The real shift isn't an exit; it's a move toward stickier, higher-trust supplier relationships in specific industrial clusters.
Another overlooked dimension is the rise of dual-layer sourcing. Brands keep final assembly in China for domestic and high-mix orders while shifting only standard, high-volume products elsewhere. This lets them use Chinese suppliers' engineering feedback to refine designs before any secondary production line starts. The result is less about derisking in the abstract and more about using China as a product development engine, not just a factory floor.
There is also a talent arbitrage taking place. Chinese suppliers are hiring veteran quality engineers from Japanese and German firms, quietly closing the gap on precision manufacturing. For buyers, this means the old assumption that China equals good enough for simple parts no longer holds. The sourcing shift to watch is not geographic but capability-based, and it is happening inside the same factories that were once dismissed as low-tier.
Finishing Lines That Run Longer Between Maintenance
Longer maintenance intervals start with how the line handles everyday wear. On newer systems, contact points like rollers and guides are often fitted with ceramic or polymer coatings that resist abrasion far better than bare steel. Add in sealed bearing housings and you remove the main reason operators used to stop for greasing every few hundred cycles.
Filtration and lubrication have also moved away from manual routines. Self-contained oil recovery and automatic misting systems keep moving parts conditioned without someone walking the line with a grease gun. This isn't about adding sensors for the sake of data; it's about designing out the small failures that used to cascade into unscheduled downtime.
The practical result is a finishing line that can push through longer production runs while holding surface quality steady. With fewer interruptions for inspection and part replacement, the same crew can handle higher output, and maintenance shifts focus from reactive fixes to planned overhauls timed around production calendars.
Hard Chrome Tanks Designed Around Your Workload
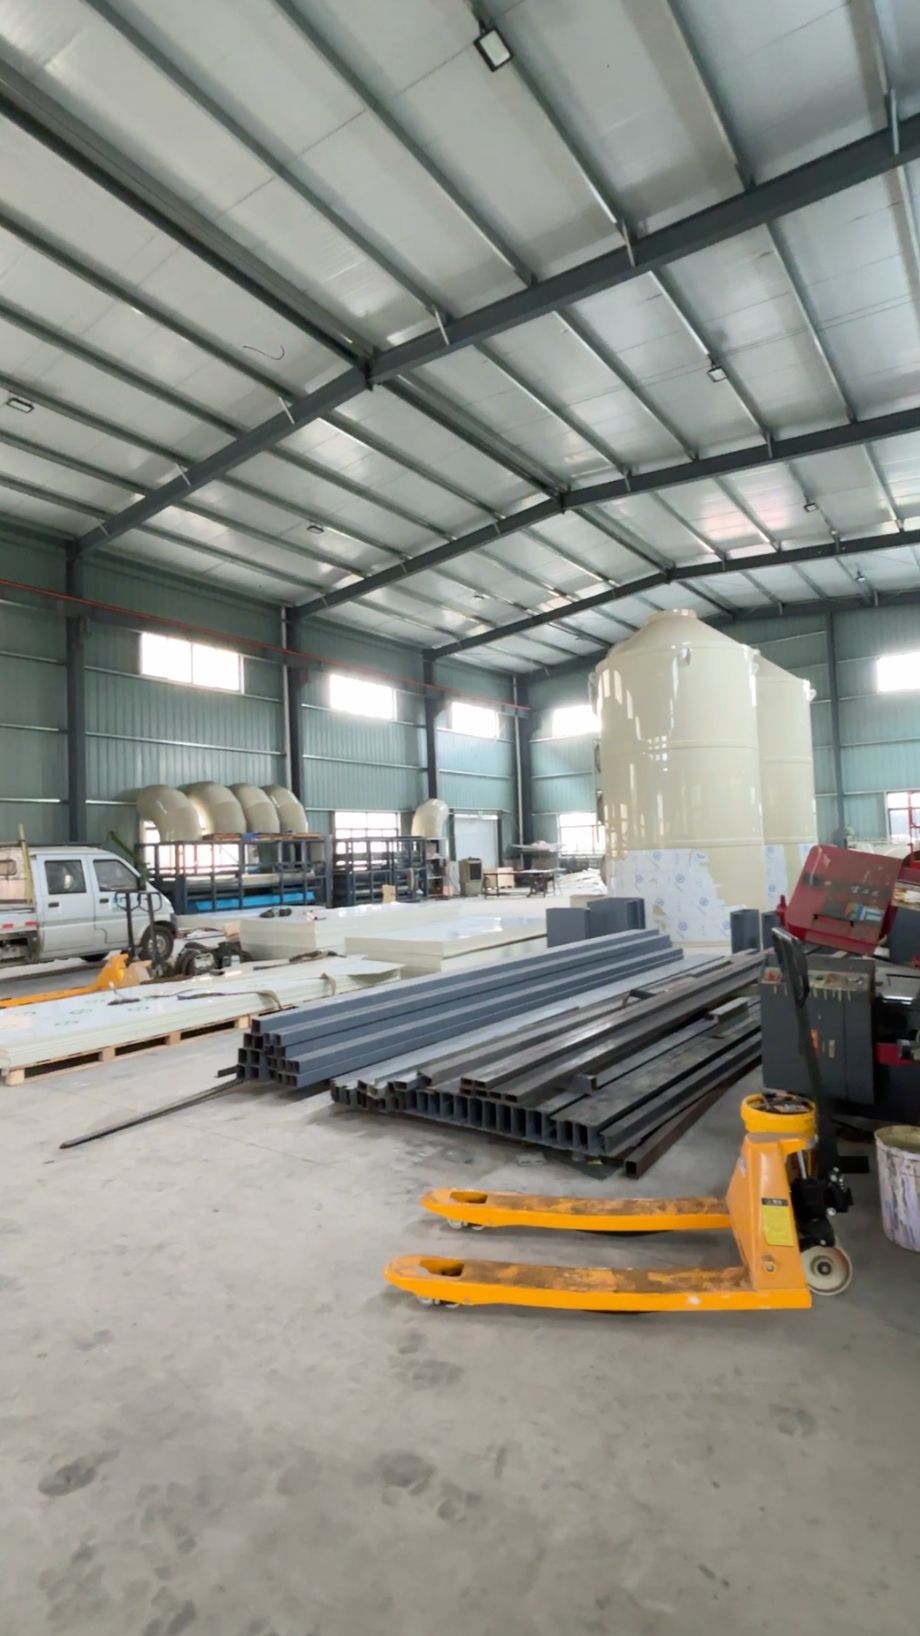
Hard chrome tanks get specified too often from a catalog size, then forced to fit real parts. We work the other way: the largest shaft, roll, or racked batch sets the working depth and width first. From there, anode spacing, rectifier bus placement, and solution agitation are laid out for the actual current density and thermal load your parts will pull.
Mixed workloads change the design quickly. A line running both long hydraulic rods and small mold details may need stepped tank depths, deeper freeboard for fast entry, or internal baffles to keep mist and drag-out contained during manual loading. Hourly throughput matters more than total volume, so heating, cooling, and filtration are matched to peak production rather than average tank capacity.
That approach avoids the usual bottlenecks: cold spots near the tank walls, starved anodes on dense racks, and rectifier capacity that cannot hold a steady ramp when the bath is full. You end up with a chrome tank that fits the lift equipment and floor space already in the shop, without buying extra length or depth you will never use.
What Trusted Finishers Look for in a Rectifier
An experienced finisher rarely gets excited about a rectifier's brochure numbers. What they actually check is whether the output stays tight under a shifting load. A machine that drifts a few millivolts during a long nickel run can leave you with visible banding on the parts. Low ripple matters just as much as rated amperage, especially for hard chrome or precious metal work where the deposit thickness has to be dead consistent. If the constant-voltage to constant-current crossover isn't clean, you'll hear about it from the platers before the day is over.
Downtime in a plating shop is brutal, so trusted finishers look hard at how a rectifier is built, not just what it promises on the spec sheet. They want access to the main board without a pile of custom tools, cooling paths that don't clog with shop dust, and terminals that a gloved hand can actually reach. A rectifier that needs a specialist from three states away for a simple fault is a liability. Modular diode stacks and clearly labeled fuses win more respect than a slick touchscreen that hides every diagnostic behind five menus.
Protection features separate a shop-ready rectifier from a lab toy. Finishers expect fast overcurrent shutdown, thermal derating that doesn't silently cook the internals, and a remote interlock that plays nice with their hoist or rectifier timer. If the unit can't survive a splash of rinse water or the occasional chemical mist, it won't last a season. The best rectifiers in a job shop are boring—they just keep delivering clean DC, shift after shift, without needing constant babysitting.
FAQ
Many finishers find that the equipment combines solid engineering with practical service life. Tanks, rectifiers, and anode systems are often built to straightforward specs and hold up under daily use, which reduces the urge to look elsewhere.
It usually comes down to how well the rectifiers control ripple, how evenly the solution is agitated, and whether the tank linings resist chemical attack. When those three are done right, the chrome deposits come out consistent batch after batch.
Yes, many suppliers will adjust dimensions, add heating or cooling jackets, and configure anode placements to match your workshop layout. The key is to send detailed drawings up front so the quote reflects what you actually need.
Most trusted suppliers include fume extraction hoods and scrubber connections as standard, and they can pair the plating line with treatment units for hexavalent chrome. That matters because local discharge limits are getting stricter almost everywhere.
Look for thickness of the tank walls, the rectifier's actual output under load, and whether all electrical connections are properly insulated. Also ask for a video of the line running a test cycle before it leaves the factory.
Increasingly, yes. You can get programmable hoists, timed current control, and even temperature logging tied to a central panel. It won't replace a skilled plater's eye, but it takes a lot of guesswork out of repeat jobs.
It varies, but the ones finishers trust tend to offer remote troubleshooting, spare parts lists with clear part numbers, and sometimes on-site commissioning engineers. Ask about response times before you place the order.
Conclusion
Industrial finishers who plate hard chrome day in and day out don't choose equipment on a whim. They look for a line that holds up when a single hour of downtime costs more than the tank itself. That's why the current wave of China-built hard chrome systems is gaining real traction among shops that used to insist on domestic names. The shift isn't about chasing the lowest quote; it's about finding fabricators who understand production rhythm, build tanks around the shop's actual workload, and size cooling, agitation, and fume control to match the parts moving through the line. When a plater can run a full week without babying a bus bar or chasing a leak, that equipment earns its place on the floor.
Where these systems prove themselves is in the details. Thickness tolerance is non-negotiable for shops handling aerospace, hydraulic, or mold work, so the rectifiers paired with these tanks matter as much as the plating cells themselves. Trusted finishers look for ripple control, stable output under load, and straightforward calibration, because a rectifier that drifts mid-run quietly ruins a batch. Longer maintenance intervals come from practical design: reinforced tank rims, properly placed anodes, and accessible plumbing that doesn't require a shutdown to inspect. Add in lead times and support that actually respond when a line is down, and it's clear why more finishing managers are treating China as a serious sourcing option rather than a compromise.
Contact Us
Contact Person: hayyr
Email: [email protected]
Tel/WhatsApp: 8613082110525
Website: https://www.jundaelectroplating.com