Best Concrete Pipe Making Equipment Factory That Delivers Consistent Quality
2026-09-19
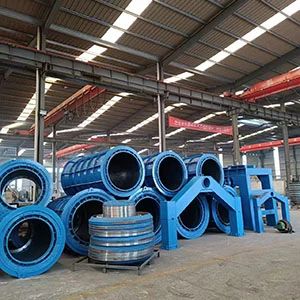
When every concrete pipe must meet exacting standards, consistency isn’t a luxury – it’s the whole game. Yet too many manufacturers still settle for equipment that drifts out of tolerance, causing costly rejects and delayed projects. That’s where Qianfeng Electromechanical Equipment changes the equation. Built for repeatable precision and long-run durability, their concrete pipe making machinery has earned a reputation among contractors who can’t afford surprises. In this post, we’ll look at what truly separates a dependable pipe production line from the rest – and why the right factory partner makes all the difference.
Raw Material Batching That Removes Guesswork from the Mix
Every batch starts with a question: are these proportions actually right? Too often, operators rely on memory, sticky notes, or a quick glance at a faded clipboard. That's where mistakes creep in—a few extra pounds of filler, a missing additive, or a rushed pour that throws the entire recipe off. Raw material batching that removes guesswork means turning those moments of uncertainty into a closed loop. The system knows exactly what each formula demands, down to the gram, and it won't let a batch proceed until every ingredient matches the spec.
Think of it as a kitchen scale with a built-in recipe book, but for industrial mixing. Operators aren't left to interpret vague instructions or double-check their own math. Instead, the batching interface guides them step by step: which silo to pull from, how much to dispense, and when to stop. If something drifts off target—say, a load cell reads 2% under the required weight—the system flags it immediately, not after the batch is already in the mixer. That kind of real-time vigilance removes the "almost right" batches that plague so many plants.
The real payoff shows up in consistency. When every batch starts from a verified, measured foundation, the downstream process doesn't have to compensate for guesswork. Mixing times stabilize, reject rates drop, and your quality team stops chasing phantom variations. It's not about adding more automation for its own sake—it's about giving operators a reliable partner that handles the exacting part, so they can focus on keeping the line moving without second-guessing the hopper.
Vibration Frequency Tuned to the Pipe’s Exact Wall Thickness
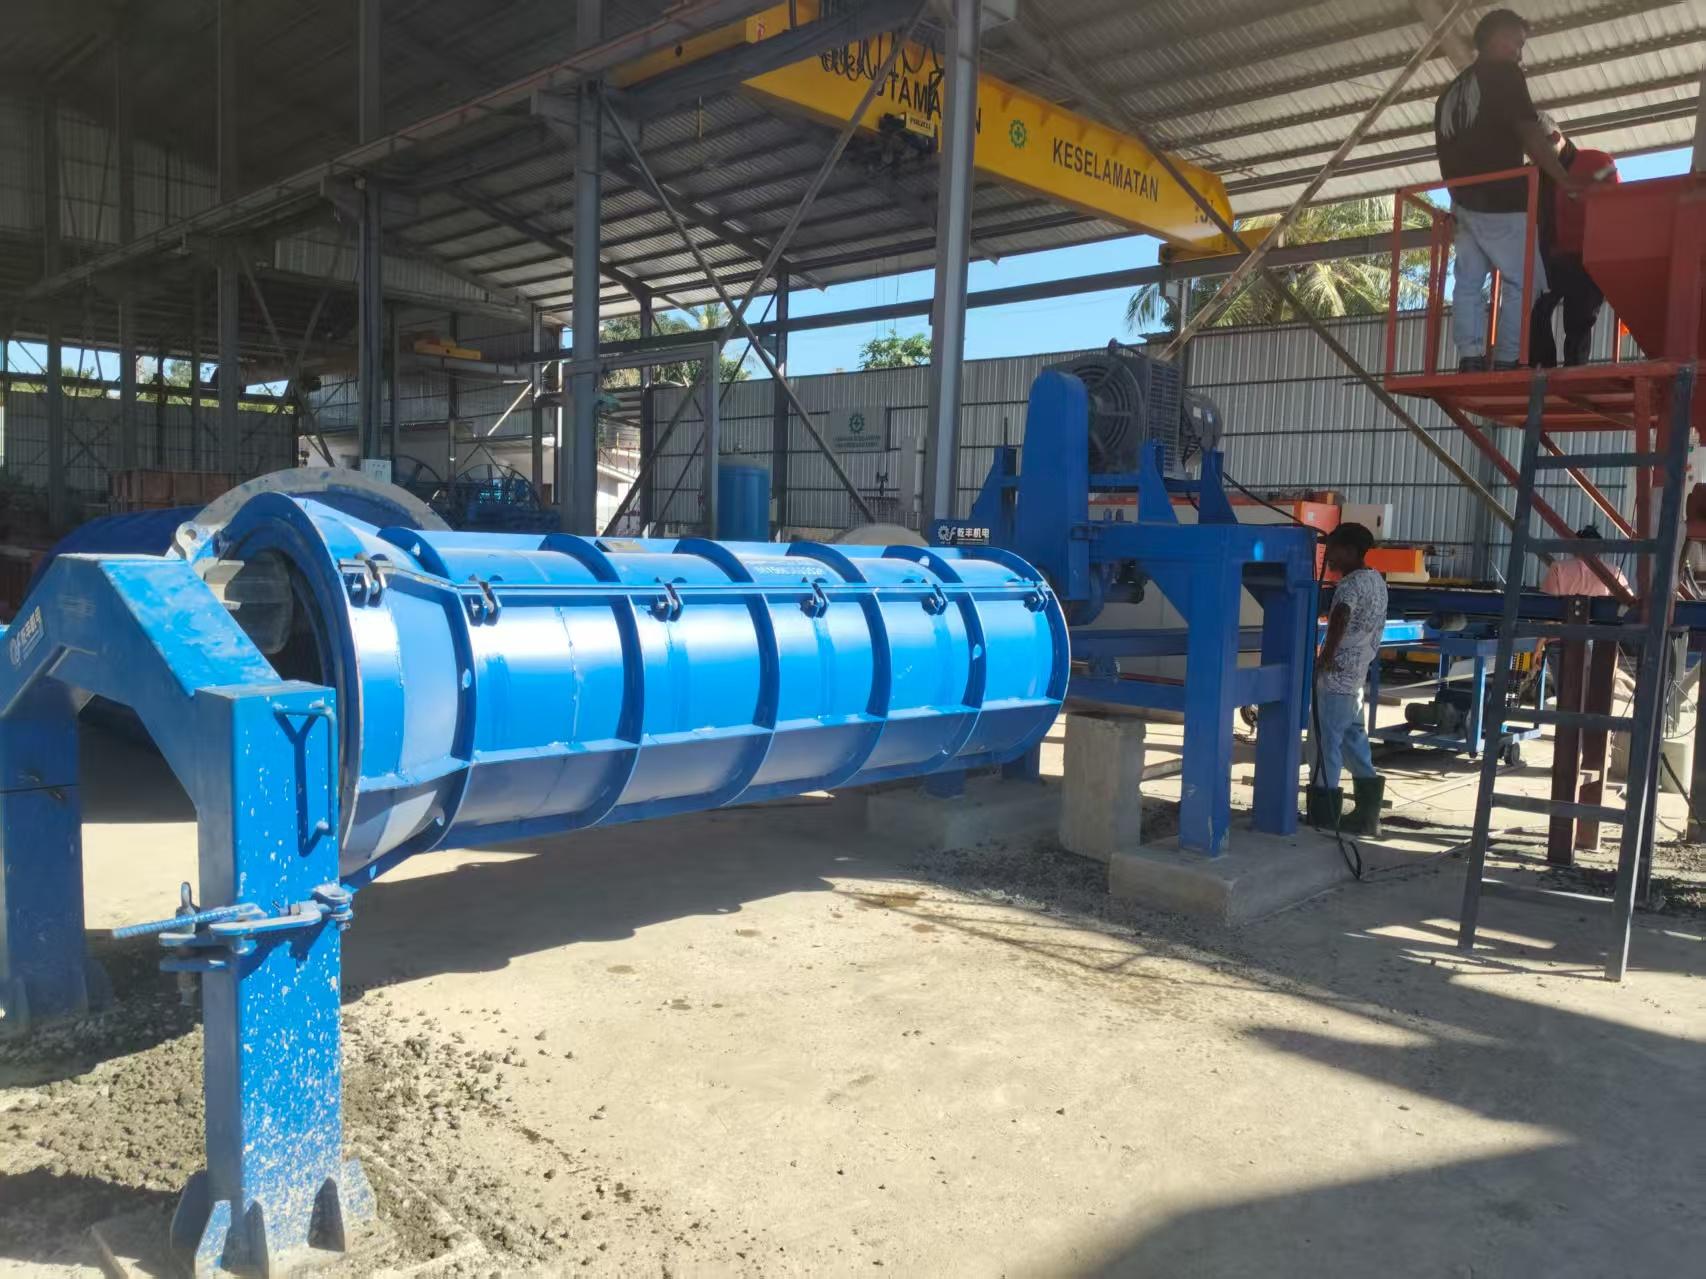
Most ultrasonic tools calibrate to a generic pipe schedule, leaving a margin of error that can hide real corrosion. This system measures the actual wall thickness at each test point first, then adjusts its excitation frequency to match. The result is a clean, center-of-resonance response instead of a blurred peak.
By locking the frequency to the pipe's exact thickness, even 0.2 mm of wall loss shifts the resonance enough to trigger an early warning. No more guessing between a thin spot and a coupling artifact. Field crews get a pass/fail signal they can trust without re-tuning between joints.
Thicker pipes ring lower, thinner ones ring higher. The frequency tuning follows that physical reality automatically, so the same probe works on schedule 40 and schedule 80 pipe without changing settings. This removes the biggest source of false negatives in conventional spot-checking.
Mold Alignment Protocols That Keep Joints Leak-Free
Achieving a leak-free joint starts long before the first shot is fired. The core and cavity inserts are seated against each other with a deliberate interference check across the parting line. Instead of relying on clamp tonnage alone, a properly aligned mold uses hardened locating rings on the stationary side and precision-ground leader pins that enter bushings without any side loading. Any visible daylight between the plates at rest means the alignment has already drifted; that gap will widen under injection pressure and turn into a flash path at the joint.
Thermal growth changes the rules once the mold reaches operating temperature. Alignment protocols that ignore this will pass a cold-room check but fail on the press. The practical fix is to clock the tie bars and check platen parallelism under full tonnage, then shim the back of the mold or adjust the clamping plate until the parting line closes evenly from corner to corner. A strip of feeler gauge drawn along the joint should meet the same resistance on all four sides—any variation is a warning that the sealing faces are no longer sharing load equally.
The final safeguard is a controlled leak test at low pressure before production speed is ramped up. Run the mold with a short shot or a slower injection profile and watch the joint closely for the first signs of polymer bleed. If a telltale line of material begins to form, stop and re-check the alignment rather than increasing clamp force to mask it. Small corrections to the guide components and platen leveling at this stage prevent the sort of chronic flashing that erodes both the tool surface and the operator's trust in the process.
Steam Curing Curves Adjusted by Ambient Conditions, Not a Fixed Timer
A preset countdown for steam curing rarely matches the way concrete actually gains strength on a job site. When the surrounding air is cold, the same heating schedule that works in summer leaves the surface lagging behind the core, and when humidity spikes, condensation patterns change how heat penetrates the form. So the control system has to read ambient temperature, concrete temperature at two or three depths, and moisture in the curing chamber before deciding how long to hold each plateau.
Instead of a fixed timer, the ramp rate is tied to the difference between the surface and the center of the section. If that gap exceeds a set limit, the steam valve throttles back even if the clock says it is time to push harder. The dwell period at maximum temperature then extends only until maturity or strength gain reaches a target that is adjusted for the day’s barometric pressure and initial mix temperature. This keeps thermal shock and delayed ettringite formation from being baked into the product.
Operators still see a schedule on the screen, but it is a live curve rather than a recipe. A cold front moving through at 4 a.m. shows up as a small flattening in the temperature ramp, not an alarm. A humid afternoon shortens the cooling phase because evaporation is slower and the surface stays warmer. Over dozens of pours, this produces less cracking, fewer rejected panels, and shorter total cycle times than any one-size-fits-all program.
End-of-Line Pressure Testing That Simulates Real Burial Loads
Typical pressure tests only push water or air through a pipe sitting on the surface. That tells you almost nothing about how the line will behave once it's under half a metre of backfill with a loaded truck rolling over it. End-of-line pressure testing flips the setup by applying a realistic external load to the pipe while the internal pressure climbs. It's not a new idea, but it's rarely done well — most crews skip it because the rig takes extra time to set up.
The test usually involves a steel frame that clamps around the pipe near the end cap, with hydraulic jacks pressing down to mimic soil weight and live loads. As the internal pressure rises to the specified rating, the side plates and top plate hold the pipe in the same position it would be in a trench. Any joint that's going to slip, any wall that's going to buckle, or any fusion seam that's weaker than the parent material shows up long before the pipe goes into the ground. That's the whole point: better to find the defect at the laydown yard than after the road is repaved.
For contractors and inspectors who have dealt with mysterious post-installation leaks, this kind of end-of-line check changes the conversation. It moves the failure point from the middle of the night on a live project to a controlled, repeatable process. The data from each test also gives you a baseline for what that specific batch of pipe can handle, not just what the manufacturer's brochure claims. When the pipe finally gets buried, you already know it survived worse.
Operator Dashboards That Flag Variation Before It Becomes a Batch Problem
On a busy production floor, small drifts in temperature, pressure, or fill weight rarely announce themselves. A dashboard that only updates every few minutes misses the early wobble that turns into a rejected batch. The best operator dashboards pull in sensor data continuously and overlay it against control limits, so a shift from baseline shows up as a visual nudge before the line ever drifts out of spec.
The trick is making variation impossible to ignore without crying wolf. Instead of dumping every raw data point on screen, these dashboards rank deviations by practical impact—maybe a subtle color change on the mixer RPM readout, a soft banner when the coating thickness mean creeps upward across the last twenty cycles. Operators can tap into a trend view for that specific parameter and see exactly when the drift started, which shift was running, and what adjustments were made nearby.
What sets a useful dashboard apart is that it doesn't just say something is changing; it gives operators enough context to act before the batch record is locked. A note that "fill weight mean shifted +0.8 g after 10:42 adjustment" beats a generic red alert every time. Over a few weeks, this kind of early flagging becomes part of the line's rhythm—catching variation while it's still cheap to correct, not after it has already become a batch problem.
FAQ
A factory that truly excels focuses on precision machining, automated batching systems, and real-time monitoring during the curing process. These elements work together to reduce variations in wall thickness and compressive strength, so every pipe that leaves the line performs the same way.
It's often the unsung hero. Proper aggregate storage, moisture control, and calibrated feeding mechanisms prevent mix fluctuations. Even small deviations in water-cement ratio can cause cracks or weak spots, so a factory that invests in accurate material handling is investing in reliability.
Yes, and that's a key indicator of a capable manufacturer. Adjustable molds, quick-change core systems, and programmable vibration settings allow switching from small drainage pipes to large culverts while keeping the same compaction and finish standards.
Reinforcement cages need to be precisely welded and centered within the mold. A factory that uses automated cage welding and laser-guided positioning reduces human error, which directly translates into pipes that meet load-bearing specifications every single time.
Through continuous monitoring and feedback loops. Advanced factories use moisture probes in the mixer and automatic water dosing adjustments. Batch records are logged and compared, so if the ambient temperature or aggregate moisture changes, the system corrects the recipe instantly.
Look beyond the final inspection. Ask about in-process checks like slump tests, vibration frequency monitoring, and steam curing temperature curves. A factory that documents these parameters and shares them openly is more likely to deliver consistent quality than one that only checks the finished product.
Worn molds, misaligned joints, and degraded vibration motors introduce subtle defects that grow worse. A factory with a proactive maintenance schedule—replacing wear parts before they fail and calibrating sensors monthly—keeps production within tight tolerances year after year.
Because concrete gains strength through controlled hydration. Factories that use automated steam curing or high-pressure autoclaves with precise temperature and humidity control avoid weak, under-cured sections. This consistency means pipes can be safely handled and installed sooner without hidden weaknesses.
Conclusion
A plant that consistently turns out dependable concrete pipe starts with raw material batching that strips out the guesswork. Moisture probes and automated weigh hoppers adjust aggregate and cement ratios in real time, so every mix arrives at the same slump and density regardless of who is running the line. That consistency carries into the forming stage, where vibration frequency is matched to the exact wall thickness of the pipe being cast—thicker walls get lower, deeper pulses while thin-wall sections use higher frequencies to avoid segregation. Mold alignment is handled with laser-guided checks and hydraulic clamping, keeping the joint faces perfectly square. The result is a spigot-and-bell connection that seats tight every time, eliminating the slow seepage that plagues poorly aligned molds.
Curing is not left to a fixed timer. Sensors track ambient temperature, humidity, and even wind speed around the kiln, then adjust steam input to maintain an optimal temperature rise and hold period. This prevents both under-cured green pipe and the brittleness that comes from too-rapid hydration. Before any pipe leaves the yard, end-of-line pressure testing loads each section to pressures that mimic real burial conditions—including live loads and groundwater head—rather than a simple bubble test. Meanwhile, operator dashboards pull data from every stage, flagging subtle shifts in mix moisture, vibration amplitude, or curing slope long before they become a full batch of rejects. That early warning loop is what separates a facility that occasionally makes good pipe from one that makes good pipe every shift.
Contact Us
Contact Person: Bill
Email: [email protected]
Tel/WhatsApp: 8615063653526
Website: https://www.qianfengjd.com